
Bulk Clothing Production: What Changes When You Move From Sample to Line
Bulk production changes the rules: fabric is committed in rolls, cutting is layered, line balance decides output, and change control disappears. Prepare for the transition.
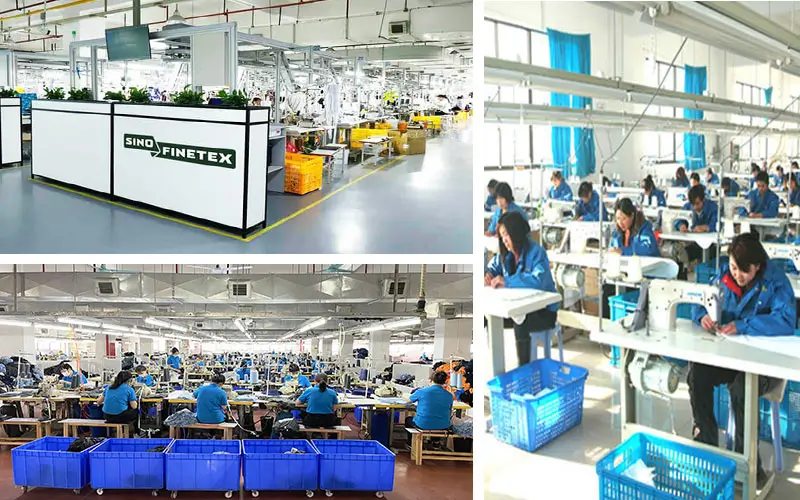
Sampling and bulk production are different operations with different economics. Sampling is flexible, small and reversible; bulk commits fabric in rolls, cuts in layers and runs to a line balance that cannot absorb late changes. The buyers who struggle are usually the ones who expected the sample-stage flexibility to continue.
What changes the moment bulk starts
Reversibility ends.
In sampling, a change costs one garment; in bulk, the same change costs every garment already cut, and the further the order has progressed the more expensive the correction becomes.
The transition happens when the pre-production sample is approved and the fabric is committed to the order. From that point, the quantities are no longer matters of one unit but of full rolls and full lays, and the decisions that were cheap to revise become expensive to revise. Fabric is bought or allocated in a quantity derived from a consumption calculation, not from the number of garments that will pass inspection. Trims are ordered to a quantity, and the elastic, labels and bags arrive in supplier lots. The line is allocated a block of machine time and a sequence of operations, and the operators learn a rhythm. Each of these is a commitment, and each of them makes a late request more costly than it would have been a week earlier.
Fabric commitment: rolls, dye lots and risk
Fabric is committed in lots that cannot be mixed freely.
Bulk fabric arrives as rolls from a dye lot, and once the cutting has begun the lot allocation is fixed, which is why shade control becomes a bulk-stage problem rather than a sampling one.
A sample is cut from a single piece of fabric and therefore never encounters the shade variation that exists between rolls. In bulk, fabric from several rolls is spread in the same lay, and the way the lots are separated determines whether the finished garments match. The cutting plan has to keep panels from one lot together within a garment, and where two lots are in use the plan should ensure that plenty of garments are cut from each rather than a few. Over-ordering the fabric is the standard protection against loss, and the extra quantity is a real cost that has to be planned rather than discovered. Where the style is a repeat, ask whether the fabric is from the same dye lot as the previous order, because a new lot is a new shade and the two may not match closely enough to ship together.
Marker making and layering at volume
The marker decides what the order actually costs.
At volume the marker is the single largest lever on fabric consumption, and the way the lay is built determines both the consumption and the cutting accuracy.
A marker is the arrangement of pattern pieces on the fabric width, and a small improvement in the arrangement produces a saving on every metre consumed across the whole order. The marker must also respect the fabric’s direction, the nap where there is one, and the size ratio the order calls for, which means the most efficient arrangement is not always the usable one. Layering introduces its own decisions: how many plies to spread, how the plies are relaxed before cutting, and how the cut pieces are numbered so that a garment is assembled from panels of the same shade. Cutting accuracy becomes more important at volume because a small deviation is repeated across every ply in the lay rather than across one sample. Ask what consumption the quotation is based on, and whether the marker will be re-made once the size breakdown is confirmed, because a marker built for a different size ratio can consume more fabric than was priced.
Line balancing and daily output
The line produces at the pace of its slowest operation.
A sewing line is balanced when the work at each station takes a similar amount of time, and where one operation takes longer than the others the output of the whole line is set by that operation.
In the sample room one person may make an entire garment, so the pace is that person’s pace. On a production line the garment moves from station to station, and the line’s output is limited by the operation that takes longest. Balance is achieved by dividing the work differently, by adding a machine or an operator at the slow operation, or by accepting the bottleneck and planning around it. The balance also changes as the line learns the style: the early output is slower because the operators are still learning, and it improves as the rhythm settles. That improvement is why an order’s delivery is usually quoted against a ramp rather than against the first day’s output. Ask how many stations are on the line, which operation is expected to be the bottleneck, and how the daily target is calculated, because the answers make the schedule testable rather than optimistic.
In-line control instead of end checks
Control moves to the operations.
Once the line is running, checking finished garments is too late and too slow, so quality control moves to the individual operations and to a defined inspection frequency.
An in-line check verifies the operation rather than the completed garment: the seam at the station where it is sewn, the neck immediately after attachment, the measurement at the point where the garment is measured. Finding a fault at the operation allows correction while the piece is still in the operator’s hands, and it also identifies the cause, which is usually the machine setting or the operator’s technique rather than the material. A finished-garment check can only reveal that the output is wrong; it cannot tell the line where the problem started. The controls worth writing into the plan are the operations to be checked, the frequency and the action taken when a fault is found. The most useful frequency is high at the start of a run, when the line is settling, and can be reduced once the output is stable.
Change control: why late requests are expensive
A late change is charged at the stage it interrupts.
Once bulk starts, a change has to be priced against what it invalidates: the marker already made, the fabric already cut, the trims already ordered and the line already balanced.
Changing a measurement after the fabric is cut means re-cutting the affected panels from new fabric, which consumes additional material and additional cutting time and can leave the original cut pieces as waste. Changing a trim after the trims have been ordered may mean the supplier’s minimum has to be paid twice. Changing the colour after dyeing is not a revision but a new dye lot. The practical discipline is to freeze the specification at the pre-production approval and to route any subsequent request through a written change process with a stated cost and a stated schedule effect, so the decision is made with the consequence visible. Where the change is unavoidable, making it early in the lay rather than late is the difference between a contained cost and a disruption across the order.
Bundling, ticketing and traceability
Number the pieces so the garment can be traced back.
Bundling and ticketing are what allow a fault found at inspection to be traced to a cutting lay, a machine or an operator, and at volume that traceability is the difference between a contained correction and a re-inspection of the whole order.
The bundle is the unit of work that moves through the line, and the ticket identifies what is in it. A system that records the style, the colour, the size, the lot and the operator at each stage allows a fault to be traced backwards to its source and forwards to every garment that shares it. That is what makes a targeted remedy possible: instead of rechecking the whole order, the factory checks the affected bundles. On an order with several colours and several fabric lots, the traceability also protects the buyer, because it can demonstrate that the shade mix was controlled rather than asserted. Ask what the numbering system records and whether the records survive the order, since a system that is discarded at packing provides no protection for a claim made after delivery.
Finishing, pressing and packing at volume
Finishing becomes a line of its own.
At volume the finishing department runs as a separate stage with its own capacity, and a bottleneck there delays the shipment just as effectively as a sewing bottleneck.
Finishing covers trimming, any washing or softening, pressing, folding, tagging and packing. Each of these has a rate, and the rate at finishing may be slower than the rate at sewing, which is why a factory that has produced the full order can still be days from being able to ship it. Pressing is often the slowest step for a product that needs shaping, and hand packing is slower than a machine pack. Where a bag, a box or a folded card is part of the specification, that assembly work belongs to finishing and consumes its capacity. Ask what the finishing rate is relative to the sewing rate, because the answer explains why the last stage of the schedule is often longer than the buyer expected. Where the finish also drives the carton, the pack specification should have been settled before production rather than during it.
Final inspection and shipment preparation
The last inspection is a decision point.
Final inspection draws a sample from the completed order and compares the result against the acceptance level in the plan, which produces a pass, a rework or a rejection rather than a report.
For the inspection to be useful it has to happen at a defined point relative to packing, and the pieces it draws have to come from across the order rather than from the cartons nearest the door. On a bulk order the findings that matter most are the ones that predict returns rather than the ones that are most visible on a table, so the plan should weight neck or elastic behaviour, measurement across the graded sizes and decoration durability accordingly. Where the result is a rework, the schedule has to absorb the correction, which is the most common reason a shipment moves. Where the result passes, the goods move to cartoning and documentation, and the carton marking should already have been agreed, since a receiving warehouse needs to identify the style, colour and size breakdown without opening every carton.
Managing a first bulk run without a fixer on site
Replace presence with a reporting rhythm.
A buyer who cannot be at the factory during production needs a reporting structure that surfaces a problem while it can still be corrected rather than at the point of delivery.
The practical structure has four elements: a confirmed production start date, a mid-run progress report with the current output and any open issues, a defined point at which the in-line findings are summarised, and a pre-shipment inspection at the agreed acceptance level. The reports need to be short and comparable, so that a slipping output is visible as a trend rather than as a surprise at the end. Where the order is the first from a factory, a third-party inspection at the pre-shipment stage is worth budgeting, because it produces an independent record at the moment when the goods can still be held. What should be avoided is a reporting structure that consists of asking for reassurance, because reassurance is not evidence and it tends to arrive in a more positive tone than the production warrants. The sampling and timeline guide sets out where these checkpoints sit relative to the sample approvals that precede them.
FAQ
What happens after the PP sample is approved?
Fabric is committed to the order, the marker is made, the fabric is spread and cut in layers, the line is allocated and balanced, and production begins with in-line checks. From this point, late changes are priced against what they invalidate.
How does bulk production differ from sampling?
Sampling is small, flexible and reversible; bulk commits fabric in rolls, cuts in layers and runs to a line balance. A change that costs one garment during sampling costs every garment already cut once bulk has started.
Why does bulk fabric come in dye lots?
Because a dye vessel holds a fixed volume and the shade is matched across the whole bath, so different production runs produce slightly different shades. Bulk cutting has to keep panels from one lot together within a garment.
How do I manage a first bulk run remotely?
Use a reporting rhythm rather than reassurance: a confirmed start date, a mid-run progress report with output and open issues, a summary of in-line findings, and a pre-shipment inspection at the agreed acceptance level. Consider a third-party inspection for a first order.
Next step for your team: send the Finetex Global team your approved specification and expected quantity, and ask how the marker, the line balance and the reporting points would be handled for your first bulk run.
Sources: ISO 9001 quality management; OEKO-TEX STANDARD 100; Better Work (ILO/IFC); Textile Exchange standards; 16 CFR Part 303 textile labelling.
For the surrounding decisions in the same programme, see the the clothing factory sourcing guide.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day