
What advanced machinery is used in underwear production: A Production-Side Explanation
A rejected underwear batch rarely fails for lack of a sewing machine. It fails because the knit ran at the wrong gauge, the dye lot moved…
A rejected underwear batch rarely fails for lack of a sewing machine. It fails because the knit ran at the wrong gauge, the dye lot moved two shades under neutral light, or the waistband was applied at a tension nobody wrote down. Underwear is the least forgiving category in men’s knitwear: the panels are small, the fabric stretches, and a 5 mm measurement drift becomes a fit complaint inside a sealed multipack. By the time a buyer sees the problem, it is already spread across a thousand pieces and a launch date has moved. This article walks a men’s knitwear line station by station – knitting, dyeing, cutting, sewing, finishing and inspection – and explains which machine controls which risk, so a specification can be built on verifiable capability rather than on price alone.
The short answer: which machines carry the weight
Men’s knit underwear runs on circular knitting machines, dyeing and stentering equipment, CAD-driven cutting, flatlock and cover-stitch sewing lines with dedicated waistband and elastic stations, plus fabric and garment inspection stations. The advanced part is not one machine; it is whether gauge, shade, tension and finished measurement stay inside tolerance across all of them. Because the pieces are small and elastic, consistency depends on calibration and locked specifications, not on sewing speed.
How demand shifts and positioning reshape the machinery you need
Machine mix follows the programme, and men’s basics programmes have moved. Cotton single jersey is no longer the default base: modal, micro modal, bamboo, lyocell and performance blends now carry a large share of new underwear and undershirt lines, and they knit, dye and shrink differently from cotton. Multipack retail and e-commerce add a second pressure, because a shade difference between two packs is a return rather than a comment. Compression and sportswear lines push elastane content higher, and elastane responds to heat-setting and recovery control rather than to sewing accuracy alone. The positioning consequence is direct. A brand selling a 3-inch trunk with a soft branded waistband needs finer gauge control, precise elastic application and careful finishing; a brand selling a 9-inch boxer brief in a heavyweight fabric needs different cutting and needle selection. Both can be produced on one floor, but not with the same settings, and not without a specification that records gauge, weight per square metre, elastane percentage and finished measurements. That record is what makes two quotations comparable.
Machine sets by product type and use case
A buyer’s product type decides which stations sit on the critical path, so the useful comparison is not a factory’s equipment list but the link between that equipment and the risk being controlled. The table below maps the main programmes to the machinery that carries their risk and the evidence to request. Women’s lingerie, moulded cup constructions and denim sit outside this scope; those programmes need different machinery, and a men’s knitwear factory should be judged on criteria and verification method rather than assumed capability.
| Programme | Equipment on the critical path | What it controls | Evidence to request |
|---|---|---|---|
| Boxer brief, 3-9 inch inseam | Circular knitting, CAD cutting, flatlock and cover-stitch, waistband station | Rise, inseam, pouch shape, seam stretch | Graded size set, measurement report |
| Multipack trunks and briefs | Shade-controlled dye lots, stenter, version-controlled cut markers | Shade continuity between batches, size consistency | Bulk fabric inspection notes, AQL 2.5 photo report |
| Performance and compression | High-elastane knit, heat-setting, flatlock | Recovery, compression level, seam integrity | Fabric test reports, elastane content record |
| Certified fibre line | Segregated fibre lots, controlled dye recipe | Claim accuracy, restricted substance limits | OEKO-TEX Standard 100, chain-of-custody documents |
The equipment behind each production stage
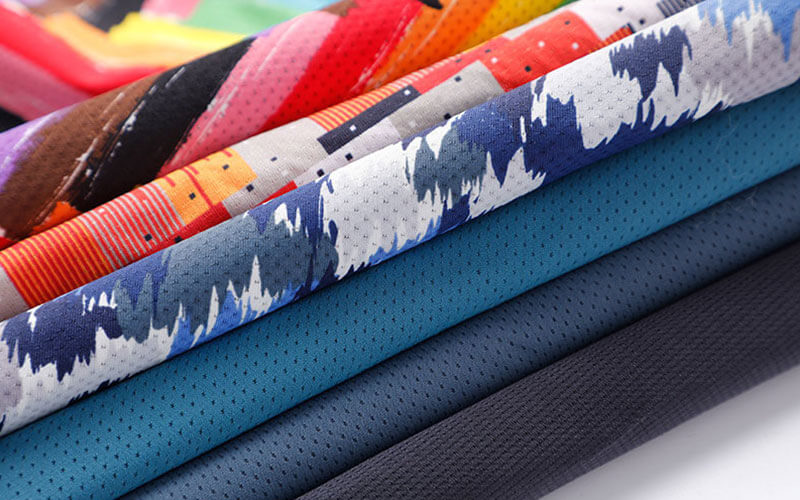
Advanced underwear production is a chain of controlled steps rather than one flagship machine. On the fabric side, circular knitting produces the tubular knit, rib and interlock structures underwear depends on; package or yarn dyeing creates stripes and yarn-dyed effects; jet or beam dyeing sets the base colour; and a stenter or compactor controls width, shrinkage and hand before a roll reaches the cutter. For Finetex Global programmes, knitting and dyeing run through long-term partner mills working to the factory’s production plan, while sampling, cutting, sewing, finishing, packing and export handling stay under one schedule inside the Shenzhen operation. Bulk fabric is inspected for shade continuity, shrinkage, weight per square metre and colour fastness before cutting starts, which is where most rejected batches are actually prevented. Cutting runs from CAD markers, sewing uses flatlock, cover-stitch and dedicated waistband and elastic stations built for knit underwear, and finishing, packing and export documentation close the line.
How Finetex Global runs its production floor
Finetex Global is the brand of Finetex Textile Co., Ltd., a men’s knitwear OEM and ODM manufacturer in Shenzhen producing for export since 2004. The operation runs 12 sewing and production lines in a 5,652 sq m factory and covers men’s underwear, undershirts, T-shirts, tank tops, polos, sweats, hoodies, loungewear, compression and sportswear – breadth that matters for machinery, because the same cutting and sewing assets serve several categories and scheduling decides how efficiently they do it. Sampling takes 5-7 working days for a fit or development sample and 10-12 working days for a graded size set, with samples built from bulk fabric where relevant, all indicative and subject to the latest quotation. Specifications are version-controlled, an approved physical sample is held by both parties, in-line QC runs at 30% and 70% of the run, and final random inspection follows AQL 2.5 with a photo report before packing. Compliance documents available on request include OEKO-TEX Standard 100 certification, BSCI or Sedex audit records, and buyer-specific testing through SGS, Intertek or Bureau Veritas.
How to specify equipment by programme type
Programme type, not machine count, should drive the specification. A value multipack runs on standard-gauge knitting with simple elastic and stock-dyed colours; a premium basics line needs tighter gauge control, softer hand and cleaner waistband finishing; a performance line needs heat-setting, recovery testing and elastane content on the spec sheet; and a certified fibre line needs segregated lots plus chain-of-custody paperwork before any claim is published. The table below compares them by fabric, equipment demand, cost driver and order size.
| Programme | Fabric and weight | Equipment demand | Cost driver | MOQ frame |
|---|---|---|---|---|
| Value multipack | Cotton or cotton-rich knit, lighter weights | Standard-gauge knit, basic elastic station, high-throughput cutting | Fabric weight, pack assembly, freight | From 300 pcs on stock fabric |
| Premium basics | Modal, micro modal or pima, mid weights | Finer gauge, soft-hand finishing, precise elastic application | Fibre price, finishing, waistband construction | Usually from 1,000 pcs per colour |
| Performance | Nylon or polyester blends with elastane | Heat-setting, flatlock, recovery control | Elastane percentage, testing, development time | Set by fabric development |
| Certified fibre | Bamboo, lyocell or recycled polyester, 120-320 gsm | Segregated lots, controlled dye recipe, documented chain | Certified fibre premium, tracing paperwork | Higher, dedicated lots |
Cost and MOQ: where fabric weight and elastane decide the number
On most men’s knit underwear programmes, fabric accounts for roughly 45-60% of unit cost, which is why weight and elastane percentage decide whether a quotation fits a retail price point long before sewing minutes do. Choosing a heavier knit rather than a lighter single jersey adds fibre cost across the whole piece, and adding elastane improves recovery while raising yarn price and making heat-setting and cutting less forgiving. Trims, waistband elastic, retail packing and freight fill most of the remainder, with labour taking a smaller share on higher-volume styles. Minimum order follows the same logic: 300-5,000 pcs per style across the range, styles using stock fabric able to start from 300 pcs, a fully custom knit or dye lot typically starting at 1,000 pcs per colour, and about a third of programmes starting below 1,000 pcs per style. All of these figures are indicative and subject to the latest quotation. Because the same lines also run undershirts and T-shirts, mixing categories in one schedule can absorb fixed setup cost – a legitimate lever when the launch quantity is small.
Tests and QC gates to run before bulk production
Four gates carry the weight that final inspection cannot recover later. Bulk fabric is checked against the approved standard for shade continuity, shrinkage, weight per square metre and colour fastness. In-line QC runs at 30% and 70% of the run, which catches waistband tension and seam problems while they can still be corrected on the line instead of at final audit. Final random inspection follows AQL 2.5 with a photo report before packing, and buyers can specify third-party testing through SGS, Intertek or Bureau Veritas under retailer or ISO 9001-type programmes. Labeling is a gate in its own right: fibre content, country of origin and care instructions must match approved artwork and the applicable rules, which in the United States fall under FTC textile labeling guidance and 16 CFR Part 303, with care symbols defined by Ginetex. A label mismatch is a compliance problem, not a cosmetic one.
How a programme starts: sampling, spec lock, bulk
A programme starts with a tech pack or reference garment and ends with a locked specification. Finetex Global reviews the pack, checks pattern and grading, matches fabric, and builds a fit or development sample in 5-7 working days, then a graded size set in 10-12, both indicative and subject to the latest quotation. Sampling corrects rise, inseam, pouch, waistband tension and measurements before bulk fabric is committed – see the boxer briefs factory page for the construction options. Once approved, specs are version-controlled, an approved sample is held by both parties, and bulk runs to that locked version. Quotations return within one working day with fabric, labour, trim and packing shown separately, stay valid for 90 days, and sample charges are credited against the bulk order. One named merchandiser owns the programme and sends weekly written updates, so schedule changes arrive as information, not a surprise.
Send a tech pack or reference garment to Finetex Global’s contact page and the team returns a costed quotation within one working day, with fabric, labour, trim and packing shown separately. Sampling runs 5-7 working days for a development sample and 10-12 for a graded set, indicative and subject to the latest quotation.
FAQ
Who is the world’s largest underwear manufacturer?
There is no single verified answer, because rankings depend on whether they count brands or contractors, revenue or units, and underwear alone or all apparel. Brand owners such as PVH, which publishes corporate disclosure, are not the same businesses as the factories that sew their goods, and contract manufacturers rarely publish comparable figures. A buyer should set headline claims aside and check audited capacity, line count, category experience, certificates and references instead. Ask any factory claiming scale for documents that tie its stated capacity to a line count and production month.
Is underwear business profitable?
It can be, but margin is decided by cost structure and channel rather than by the category itself. Fabric usually represents 45-60% of unit cost, so fibre choice, fabric weight and elastane percentage move profitability more than sewing efficiency does. Returns, multipack price points, freight and duty then decide what remains. A brand modelling a programme should build from a quotation that separates fabric, labour, trim and packing, and test the plan at both a low and a high return rate before committing to a launch quantity. Volume discounts only help when the added units sell through.
What types of machines are used in the textile industry?
The machines split by stage rather than by product. Spinning frames turn fibre into yarn; circular and flat knitting machines make the fabric; dyeing and finishing ranges set colour and hand feel; spreading and cutting machines prepare panels. Sewing lines run lockstitch, overlock, flatlock and cover-stitch machines, with bartack and elastic-application stations for underwear, and printing, embroidery, washing, pressing and inspection equipment finish the garment. Automation concentrates at spreading, cutting, elastic feeding and inspection, where consistency matters more than raw speed.
Share the style you are working on, the quantities you are planning and the market you sell into. Finetex Global replies within one working day with a costed breakdown covering fabric, labour, trims and packing, plus a sampling plan: contact Finetex Global.
Related resources
- Men’s underwear manufacturer: OEM and ODM production
- Boxer briefs factory: inseam, pouch and waistband options
- Planning a heavyweight and thermal undershirt winter SKU
- Custom fabric development for knit apparel programmes
For the surrounding decisions in the same programme, see the underwear fit and fabric specifications.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day