
What is the difference between polyester and fleece: A Production-Side Explanation
A brand sends a tech pack describing a hoodie as polyester fleece. The quotation comes back with one unit price, the lab report on the bulk…
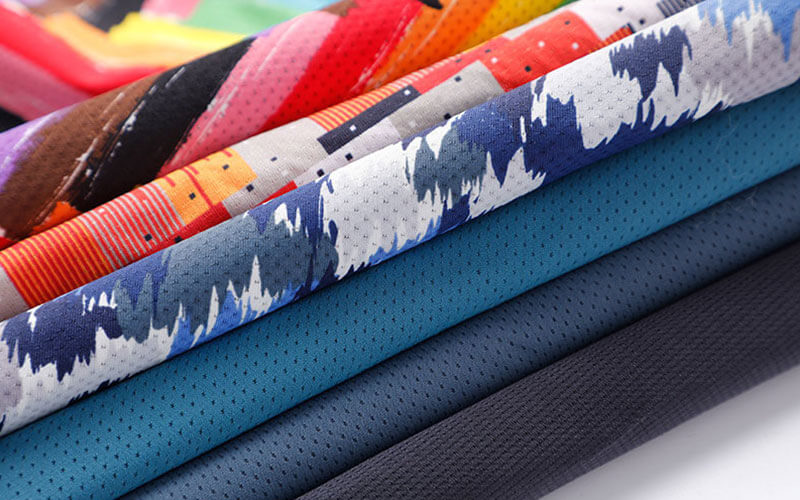
A brand sends a tech pack describing a hoodie as polyester fleece. The quotation comes back with one unit price, the lab report on the bulk fabric comes back at 100% polyester, and the competitor garment the buyer is chasing turns out to be a cotton-rich loopback that the brand’s customers also call fleece. No single document is wrong, and the range plan stalls anyway, because the words are being read at two different levels.
Polyester is a fibre. Fleece is a knitted fabric with a brushed or napped face, and it can be built from polyester, cotton or a blend. This article explains what that distinction changes on the specification sheet, in the MOQ route, in the cost breakdown, and at the QC gates a programme passes before the first bulk cut.
The short answer: polyester is a fibre, fleece is a fabric structure
Polyester is a synthetic fibre made from polymer, while fleece is a knitted fabric with a brushed surface that traps air. Fleece can be made from polyester, cotton or a blend, so a garment described as fleece is not automatically polyester, and a polyester garment is not automatically fleece.
MOQ, ready-to-ship fabric and custom logo runs on a polyester programme
First orders stall on fabric status more often than on decoration. A fleece hoodie in a shade the fabric partner already runs can move at low volume; the same garment in a brand-owned colour has to be knitted and dyed as a lot before a single piece is cut, which is a decision made weeks before a logo placement is discussed.
The two words sit at different levels of a specification. Fibre content governs care behaviour, drying speed, pilling tendency and the wording that goes on the label. Construction governs warmth, drape, weight and how the surface feels against skin. A 100% polyester interlock undershirt and a 100% polyester brushed fleece hoodie carry the same fibre entry on paper and behave nothing alike in wear.
Weight is where the confusion turns into money. Across men’s knitwear programmes the working band runs from roughly 120 to 320 gsm, with heavyweight fleece builds quoted around 420 gsm French terry and 500 gsm brushed fleece. Brushing is a finishing step applied to a base knit, so the word fleece alone does not set the price.
Write fibre content and fabric construction as two separate lines in the tech pack before anything else is finalised.
MOQ therefore follows the fabric route. Men’s knitwear programmes are quoted from 300 to 3,000 pcs per style in mixed sizes, with styles built on stock fabric able to start from 300 pcs and a fully custom knit or dye lot usually starting at 1,000 pcs per colour. Around a third of programmes booked start below 1,000 pcs per style. All figures are indicative and subject to the latest quotation.
Custom logo work, whether printing, embroidery or a woven label, is quoted as its own line and does not change the fibre specification, although a brushed polyester face prints and embroiders differently from a flat cotton jersey.
Put the decoration specification into the sampling request, not into the purchase order.
One-stop production for custom and in-stock builds: where fleece programmes break
Polyester fleece programmes rarely fail at the sewing machine. They fail where a shade decision, a grading decision and a printing decision were made by three different suppliers against three versions of the same specification.
When fabric sourcing, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation run under one production plan, those decisions answer to one locked reference instead of being renegotiated at handover. Finetex Global has manufactured men’s knitwear for export from Shenzhen since 2004, beginning as a sewing workshop, with the first programmes for European importers running from 2009 and an in-house R&D centre for fabric structure and functional knits from 2014. Fabric knitting and dyeing run through long-term partner mills, so ask any supplier describing production as one-stop which steps sit inside the factory and which are managed through partners.
Sampling runs about 5 to 7 working days for a fit or development sample and 10 to 12 working days for a graded size set, subject to the latest quotation. Where a range covers fleece, T-shirts and men’s underwear on one plan, fabric standards and inspection criteria stay aligned instead of being rebuilt per category.
Reading a fleece line sheet by construction, not by the fabric name
The construction word predicts behaviour, the fibre word predicts care and labelling, and the gsm number predicts cost. Buyers who treat all three as one field lose the ability to compare quotations, because a brushed polyester build at 500 gsm and a loopback polyester-cotton build at 300 gsm can both be filed under fleece while sitting in different seasons and price bands.
Mechanically, brushing lifts fibres from the inner face of the knit and leaves a napped layer that holds still air, which is why a lighter brushed fleece can feel comparable to a heavier unbrushed loopback. French terry carries loops on the inside and stays unbrushed unless the specification says otherwise. Jersey and interlock are flat-faced, so they move air and moisture differently again. Use the comparison below to separate the entries before the tech pack is locked.
| Entry on the spec sheet | What it is | Typical weight band | Warmth mechanism | Common volume route | Where it usually lands |
|---|---|---|---|---|---|
| 100% polyester jersey or interlock | Synthetic fibre, flat-faced knit | Light to mid | Minimal air trapping | Stock fabric from 300 pcs | Undershirts, base layers, warm-climate tops |
| 100% polyester brushed fleece | Synthetic fibre, brushed inner face | Heavy, up to a 500 gsm build | Napped surface holds still air | Usually a custom knit or dye lot from 1,000 pcs per colour | Cold-season hoodies and sweats |
| Polyester-cotton blend fleece | Blended fibre, brushed knit | Mid to heavy | Napped surface, softer hand | Stock shade or a custom lot | Retail sweats with a cotton story |
| Cotton or cotton-rich fleece | Natural fibre, brushed knit | Mid to heavy | Napped surface, more fibre weight | Usually a custom lot | Premium and heritage-fleece ranges |
| French terry, loopback | Construction defined by unbrushed loops | Mid, up to a 420 gsm build | Air layer in the loop, breathable | Stock fabric from 300 pcs, or a custom lot | Spring and autumn hoodies |
| Performance polyester knit | Synthetic fibre, engineered flat or mesh structure | Light to mid | Heat release over insulation | Depends on the base knit held by the mill | Sport and training ranges |
Treat the columns as linked decisions. A heavy brushed entry raises the fabric bill and then raises returns if it is sold into a humid market, and a flat polyester entry sold into a cold market needs a layering story to justify its place on the rail.
In-stock fleece versus OEM and ODM development: what ready to ship changes
In-stock availability compresses a calendar and constrains a colour palette. A held shade can put a hoodie on a launch date; a shade that has to be dyed gives the brand its own colour and moves the first delivery out by the length of a mill run.
Stock programmes draw on fabric held for running production, so the technical work sits in trimming, printing, packing and sizing. OEM and ODM work starts from a tech pack, a reference garment or a competitor sample and runs through pattern making, grading, fit correction and fabric matching. The boxer briefs factory pages show how a base knit is specified against a graded pattern, which is the same logic applied to a fleece body.
Before building a range plan, ask for the fabric status of every colour on the line sheet. ODM development usually carries the lower volume threshold, since the specification already exists, while a new custom knit or dye lot typically starts at 1,000 pcs per colour. Figures are indicative and subject to the latest quotation.
Price the two routes against the same delivery window before choosing between them.
Pullover fleece hoodies: where the polyester percentage changes the specification
On a pullover, the polyester percentage is a cost, weight and face decision rather than a marketing label. A higher polyester share supports loft and faster drying at a lower material cost than cotton, and it resists the fibre swelling that shows up as shrinkage on a heavy cotton fleece. A cotton-rich blend buys a softer hand and a different retail story at a higher fabric bill.
The construction underneath decides how that percentage performs. Brushed inner faces trap air and read warmer at a given weight, unbrushed loopback breathes more, and ribbing at the cuff and hem behaves differently again once elastane enters the blend. Elastane improves recovery after wear and wash, and it adds both cost and a stability that has to be checked rather than assumed.
Heavyweight pullovers are quoted around a 420 gsm French terry build and a 500 gsm brushed fleece build, both indicative and subject to the latest quotation, and the difference between them is a finishing route as much as a fibre choice.
State the fibre tolerance as a range, not a single figure, and name the wash cycle the end customer is expected to use.
Matching the fibre to the programme type: value, premium, performance and recycled
Each programme type has a default answer, which is why the fibre question resolves faster once the range is labelled honestly. A value programme wants the lowest total weight that still reads as a fleece, which usually means a polyester-rich brushed build in a held shade and the shortest route to a 300-piece order. A premium programme wants weight and face, so a heavyweight brushed build or a 420 gsm French terry on a custom dye lot carries the retail price better than an entry-weight fabric with added decoration.
A performance range inverts the fleece logic and specifies polyester for moisture movement rather than insulation, choosing a flat or mesh structure with low loft and no brushing. A recycled range is settled by paperwork before fabric, since chain-of-custody documents have to exist for a recycled polyester claim before it appears on a hangtag. OEKO-TEX Standard 100 is the material-safety reference most retailers request, and the certificate scope belongs in the order file before the claim is published.
Write the range type into the tech pack as its own line and check each claim against a document rather than against a brief.
Cost and MOQ breakdown: fabric at 45 to 60% and the gsm-versus-elastane trade
Fabric is the largest single line in a fleece quotation, typically occupying 45 to 60% of unit cost, with labour, trim and packing following. That is why swapping a brushed face for an unbrushed one shifts a quotation less than adding 100 gsm across an entire garment, which raises the material bill far more.
A quotation should show those lines separately, because a single unit price hides whether the saving came out of the fabric, the finish or the inspection routine. Costed quotations arrive within one working day and are held for 90 days. Sample charges are credited against the bulk order.
Three specification decisions drive the variation: total garment weight sets the material bill, elastane at cuff and hem improves recovery but adds cost and a stability check, and finishes such as washing or spray dyeing change yield as well as fabric behaviour. Volume follows the same logic, from 300 pcs on stock fabric to a custom dye lot usually from 1,000 pcs per colour, all indicative and subject to the latest quotation.
Quote two candidate builds in one colour so price and hand feel arrive together.
Pre-bulk testing and QC gates for polyester and fleece programmes
Most fleece complaints after shipment, including a face that pills at the cuff, a shade that drifts across a size run or a body that shrinks after the first domestic wash, were either visible in the bulk roll or predictable from the documentation. The gates sit before cutting, not at the loading dock.
Two documents make those gates enforceable. The first is a version-controlled specification with an approved physical sample held by both parties, the reference a dispute is settled against. The second is the test set: fibre composition and chain-of-custody documents for claimed fibres, colour fastness and shrinkage reports, country-of-origin paperwork, and buyer-specific testing through SGS, Intertek or Bureau Veritas.
In production, bulk fabric is inspected for shade continuity, shrinkage, weight per square metre and colour fastness before cutting, in-line checks run at roughly 30% and 70% of the run, and final random inspection is AQL 2.5 with a photo report before packing and shipment.
Care labelling belongs in pre-production approval rather than artwork stage, since care symbols follow the ISO conventions published by GINETEX and a failing label can hold a shipment that is otherwise finished.
From sampling to specification lock to bulk: starting the programme
Start with a document rather than a price. A tech pack, an existing garment or a competitor reference that states fibre content, fabric construction, target weight and finishing produces a costed quotation within one working day, with fabric, labour, trim and packing shown separately.
A fit or development sample runs about 5 to 7 working days and a graded size set about 10 to 12 working days, both indicative and subject to the latest quotation and to fabric status at booking. The pattern is graded once and locked, so bulk runs against a fixed reference, with weekly written production updates covering fabric, cutting, sewing, printing and finishing.
Final AQL 2.5 inspection with a photo report happens before packing, and one named merchandiser holds the order file, where the difference between polyester and fleece becomes an auditable line item.
Send a tech pack, a reference garment or a competitor sample with fibre content, fabric construction and target weight stated separately. A costed quotation with fabric, labour, trim and packing shown individually comes back within one working day, together with a sample plan for the build under consideration. Start at https://www.finetexglobal.com/contact-us/.
FAQ
Why do people avoid polyester?
The common objections are heat, static, odour retention and pilling, and each of them traces back to a specification rather than to the fibre family. A tight flat polyester knit worn in humidity holds sweat against the skin because the structure moves very little air; a brushed or mesh version of the same fibre behaves differently. Low-grade polyester can pill where a finer yarn does not. Performance and recycled polyester ranges exist for exactly these reasons, so the practical route is to specify the structure and test the garment instead of rejecting the fibre by name.
What fabrics to stay away from?
There is no universal banned list, and any supplier offering one is guessing about your end use. The materials worth avoiding are the under-specified ones: blends where the composition is quoted as a range with no tolerance, heavy builds with no shrinkage report, brushed faces with no pilling data, and shades held without a lot reference. Ask for fibre composition, weight per square metre, colour fastness and shrinkage results before the order is placed. A fabric with paperwork can be evaluated; a fabric without it can only be hoped for.
Is fleece always 100% polyester?
No. Fleece is a construction, so it is made in cotton, cotton-rich blends, polyester and polyester-cotton blends, and some versions carry a small elastane content for recovery. Composition is a labelling matter rather than a marketing one, and in the US market it falls under the Textile and Wool Acts as set out in the FTC textile labelling guidance and 16 CFR 303. Ask the mill for the composition with a stated tolerance and keep that record with the approved sample.
Which is warmer, fleece or polyester?
Fleece is normally warmer for the same weight, because the comparison is between a structure and a fibre. Polyester is a fibre, and fleece is usually polyester or a polyester blend built with a brushed or looped pile that traps air, which is what insulates. A plain polyester knit of the same weight feels cooler and flatter because it holds less still air. Weight decides most of the outcome, so compare grammes per square metre, pile depth and any backing, then check warmth after laundering rather than on the sample bench alone.
Share the style you are working on, the quantities you are planning and the market you sell into. Finetex Global replies within one working day with a costed breakdown covering fabric, labour, trims and packing, plus a sampling plan: contact Finetex Global.
Related resources
- Custom fabric development for knitwear programmes
- Men’s underwear manufacturing at Finetex Global
- Boxer briefs factory and knit construction reference
- Sustainable underwear manufacturing: proof and premium positioning
For the surrounding decisions in the same programme, see the the hoodie manufacturing guide.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day