
Who are the leading underwear manufacturers in China: supply chain and sourcing explained for buyers
A buyer shortlists four suppliers that appear side by side for the same search, sends the same tech pack to each, and gets back four numbers…
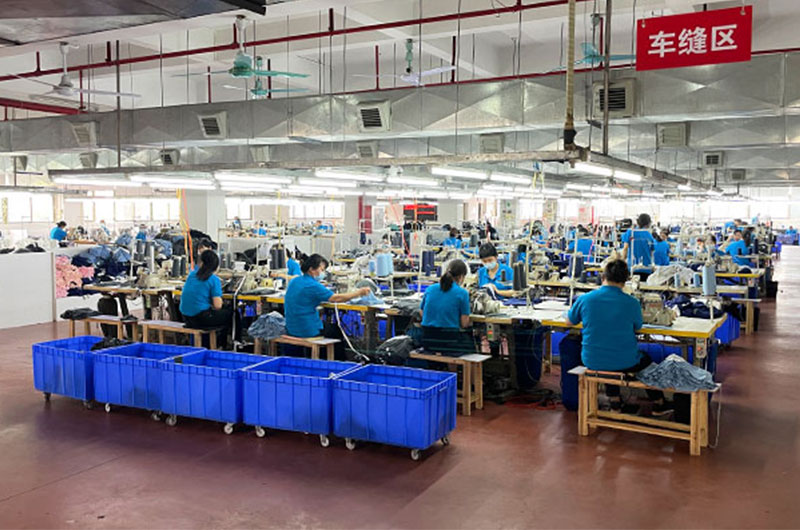
A buyer shortlists four suppliers that appear side by side for the same search, sends the same tech pack to each, and gets back four numbers that cannot be compared. One quotes a stock-fabric run from 300 pieces, another insists on a 1,000-piece dye lot per colour, and a third cannot say who knits the jersey or who signs the shade band. The gap surfaces in the second batch, half a size wide at the waist or two shades dark against the approved sample, with a retail launch pushed behind it. China’s underwear supply base is not a league table of names; it is a set of production models, and each model prices risk differently. This guide explains how that base is structured, what separates a documented factory from a well-presented one, and which checks turn a supplier list into a sourcing decision.
The short answer: how China’s underwear supply base is actually structured
Direct answer: China’s underwear supply base runs through four production models: cut-and-sew workshops, specialist men’s knitwear factories, vertically integrated OEM/ODM manufacturers, and trading companies that broker third-party capacity. No single supplier fits every buyer, because fabric choice, order volume, QC evidence and launch date decide which model works.
Unique, professional, quality: what those three labels actually verify
Those three adjectives have no fixed meaning in manufacturing; what they verify is documentation. A supplier can call a programme professional and still return a batch that sits half a size off or a shade dark, because nothing was version-controlled between the approved sample and the fabric that reached the cutting table.
Disclosure: Finetex Global (legal entity Finetex Textile Co., Ltd.) is a Shenzhen-based OEM/ODM manufacturer of men’s knitwear, including underwear, undershirts and tops, and appears as one example of the vertically integrated model, not a ranked entry. It makes no production claim outside men’s knitwear; for women’s lingerie, denim and other categories, the criteria below apply as an evaluation and verification method.
The four models differ in what they control. A cut-and-sew workshop takes your fabric and your pattern, and rarely tests bulk fabric before cutting. A trading company adds a margin and a communication layer, and may not carry specification history between orders. A vertical plant that samples, cuts, sews and packs under one production plan creates fewer handovers, and handovers are where shade and size drift enters a programme. Ask which model a supplier runs before you compare unit prices.
The verifiable version of the claim is a chain of artefacts. Specifications are version-controlled, so the revision quoted is the revision cut. An approved physical sample is signed and held by both parties. Bulk fabric is inspected before cutting for shade continuity, shrinkage, weight per square metre and colour fastness. In-line inspection runs at roughly 30% and 70% of the run, and a final random inspection at AQL 2.5 closes with a photo report before shipment. Each gate catches a problem while a roll or a cut panel can still be replaced. The workflow is set out on the capabilities page.
Practical test for any shortlist: ask for the current specification revision, the sealed approved sample and the most recent inspection report. Quotations far below the field usually trim these stages rather than operate more efficiently.
OEM and ODM underwear manufacturing: who owns the pattern and who carries the risk
OEM and ODM are separated by pattern ownership, which decides cost, speed and exclusivity. In an OEM programme you supply the tech pack, the fit belongs to you, and the factory builds to your specification. In an ODM programme you start from a block the factory owns and reach production sooner, in exchange for less exclusivity.
The consequences are concrete. A custom pattern needs fit correction before bulk, which adds a sampling cycle and a graded size set. A library block moves to a graded set once fabric and trim are agreed, so a first order reaches the line earlier. Finetex Global covers tech-pack review, pattern making, grading, fit correction and fabric matching inside product development for men’s knitwear.
Choose the model before requesting a price, because minimum order quantity, sample charge and lead time differ between the two, and every figure is indicative until confirmed in the latest quotation. Pattern and design ownership should be agreed in writing. The trade-offs between one factory plan and a split supplier network are worked through in this guide to structuring a clothing supply chain.
Men’s underwear manufacturing in China: what is actually made and where capacity sits
China’s men’s knitwear capacity clusters along the coast, and Shenzhen is one of the denser clusters for men’s basics. Product scope decides fit more than geography: a factory running underwear weekly handles waistbands, leg openings and pouch construction differently from one that adds boxer briefs to a T-shirt line.
A men’s underwear programme covers boxer briefs with 3 to 9 inch inseams and a contour or standard pouch, trunks, briefs in classic and low-rise cuts, plus jockstraps and thongs. Fabric choice spans cotton, pima cotton, modal, micro modal, Lenzing modal, bamboo, lyocell and TENCEL, nylon and polyamide, polyester, recycled polyester and performance blends, typically 120 to 320 gsm. Men’s underwear manufacturing at that breadth is hard to match.
Numbers on the specification make that scope usable: inseam and rise are graded separately, weight per square metre is a band rather than a single figure, and a leg-opening tolerance that looks trivial at sample stage is what a multipack passes or fails at retail. Ask which fabrics are stock and which need a custom knit or dye lot, because that answer sets the minimum order quantity.
What a men’s underwear catalogue has to state before it can be quoted
A catalogue is only useful when it lists the variables the order will later be held to. A photo, a price and a fabric name are not a specification, and a supplier working from them is guessing at the same time you are.
Six fields do most of the work for men’s underwear: inseam length, rise, pouch construction, waistband width and elastic type, fabric with its weight per square metre, and the size grading chart with tolerances. Add the approved shade band, because colour is the variable most likely to break between batches. Inseam and rise are related but not interchangeable, which is why 3 inch and 9 inch boxer briefs graded from one block behave differently at the leg opening.
Where a catalogue shows only a style reference, request the specification sheet behind it. A factory that can send a controlled sheet with tolerances will also be able to explain a deviation later in the run. The working rule: if a style cannot be described in those six fields, it cannot be quoted reproducibly.
OEM and ODM for your custom request: from reference garment to locked specification
A custom request becomes a manufacturable programme in five steps: tech-pack review, pattern making, grading, fit correction and fabric matching. Whether you start from a sketch, a competitor sample or a garment from your own line, the goal at the end of that sequence is one locked specification that both parties hold.
Sampling supplies the timing. A fit or development sample typically takes 5 to 7 working days, and a graded size set typically takes 10 to 12 working days, with samples built from the bulk fabric where that affects how the garment behaves. Sample charges are normally credited against the bulk order, which stops a fit-approval round from becoming a separate project cost. Timings remain indicative; the specification is locked only when the approved sample and the written revision agree.
That lock is the purpose of the exercise. Once pattern, fabric, elastic and tolerances are frozen, a reorder repeats without renegotiating fit, and a bulk run is judged against a document rather than against memory.
Sourcing by project type: value, premium, performance and eco programmes
One factory can serve four different briefs, and the brief you pick sets the fabric, the minimum order quantity and the testing plan. Sorting the programme by type before sampling avoids paying for premium fibre on a test run, or locking a value price into a fabric you cannot reorder.
A value programme lives on stock fabric, usually cotton jersey or a cotton blend at the lighter end of the 120 to 320 gsm range, with single-colour waistband branding. A premium programme moves to pima cotton, modal, micro modal, Lenzing modal, lyocell or TENCEL, and generally needs a custom knit or dye lot from about 1,000 pieces per colour. A performance brief works in nylon and polyamide, polyester, recycled polyester and performance blends, where moisture management and recovery testing matter more than hand feel.
An eco brief runs on bamboo, organic cotton or recycled polyester and depends on traceability: fibre composition and chain-of-custody documents, plus OEKO-TEX Standard 100 for the material itself. Changing fibre after the sample is signed resets both the minimum order and the grading, so make the type decision first.
Cost and MOQ: where the quotation number actually comes from
Two quotations for one style rarely match, because each embeds a different fabric share, order size and set of checks. Fabric is normally the largest single line, at roughly 45 to 60% of the ex-works unit cost, so a specification change moves the total more than a negotiation does. Figures are indicative and subject to the latest quotation.
Order size spreads development across the run. Men’s underwear programmes typically run from 300 to 3,000 pieces per style in mixed sizes: stock fabric can start from 300 pieces, a fully custom knit or dye lot usually starts at 1,000 pieces per colour, and around a third of programmes begin below 1,000 pieces per style. Weight and stretch are the other levers. A heavier weight per square metre raises fabric consumption and adds sewing time at the waistband and leg openings, and raising elastane content lifts cost while changing recovery, so both belong in the specification.
| Route | Typical fabric | MOQ stance | Where cost moves | Fits which programme |
|---|---|---|---|---|
| Stock knit | Cotton jersey or cotton blend | From 300 pcs per style | Fibre price, weight per square metre, cutting time | Value ranges and test runs |
| Custom dye lot | Cotton-modal or modal blend | Typically 1,000 pcs per colour | Dye route, shade control, sewing time | Core retail ranges and multipacks |
| Premium fibre | Pima cotton, micro modal, Lenzing modal, lyocell | Custom knit from about 1,000 pcs per colour | Fibre cost, finishing, branded waistband | Premium and gift-ready lines |
| Performance | Nylon or polyamide, polyester, blends | Quoted per style and fabric | Fabric engineering, zoning, testing | Sport and compression ranges |
| Certified eco | Bamboo, organic cotton, recycled polyester | Set by chain-of-custody lot size | Certification documents and traceability | Claim-led sustainability ranges |
Ask for the breakdown with fabric, labour, trim and packing shown separately. Finetex Global issues that quotation within one working day and holds it for 90 days, which makes re-quoting a specification change straightforward.
Pre-production testing and QC gates that catch a rejected batch early
Quality is bought at the specification stage, and the gates that protect a run cost far less than the batch they stop from shipping. A documented sequence also removes the argument about what acceptable means, because each checkpoint reports against the approved sample and the current revision.
The sequence starts before cutting. Bulk fabric is inspected for shade continuity, shrinkage, weight per square metre and colour fastness, since a roll that fails any of those four cannot be fixed by sewing. In-line inspection then runs at roughly 30% and 70% of the run. The run closes with a final random inspection at AQL 2.5 and a photo report before packing and shipment. Buyer-specific testing, where a retailer requires it, runs through SGS, Intertek or Bureau Veritas.
Labelling sits alongside testing, because a correct garment with a wrong care or fibre label is still a rejected shipment: FTC guidance on textile labelling and 16 CFR Part 303 govern United States fibre disclosure, while GINETEX symbols are the reference for European care labelling. Keep those documents in the order file before any claim is published.
How to start: sampling, spec lock, then bulk production
The path from enquiry to bulk is short when the sequence is respected and expensive when it is reversed. Sampling first, then specification lock, then bulk gives you three points at which a change is cheap and a fourth at which it is not.
Send a tech pack, a reference garment or a competitor sample with the fabric direction and target volume. Development runs through pattern making, grading and fit correction; the fit or development sample typically lands in 5 to 7 working days, with a graded size set following in 10 to 12 working days. Once that sample is approved, the specification is locked as a version-controlled document with tolerances, and bulk is cut against it. Bulk lead time is confirmed with the quotation rather than assumed, and export paperwork covers country of origin and customs documentation; destination requirements are set out in the US Customs and Border Protection import and export guidance.
Request a costed quotation from Finetex Global with fabric, labour, trim and packing listed separately, or send your tech pack for review.
FAQ
Which is the best underwear brand in the world?
No shared metric sits behind that question, which is why published rankings tend to measure marketing reach and retail turnover rather than manufacturing control. A buyer can compare something more useful: whether fibre and care information is accurate, whether sizes hold between batches, and whether the production route is traceable. Brand size and product quality are separate variables, and a large brand may run on the same contract manufacturing model as a small one. Judge the specification rather than the logo.
Who is the best clothing manufacturer in China?
That depends on the garment, the volume and the evidence you need, so a single name would mislead. The workable screen is category depth, documentation and commercial fit: does the factory run your garment type weekly, can it show version-controlled specifications and recent inspection reports, and does its minimum order quantity sit near your first order rather than far above it. Apply the same four questions to every shortlisted supplier and compare the answers side by side.
What is the leading Japanese undergarment brand?
Japan’s intimates market is served by long-established domestic apparel groups and specialist labels rather than one dominant name, and they sell through different channels. For a sourcing decision the more useful point is that brand nationality and manufacturing origin are separate: a Japanese label is often produced by contract factories elsewhere in Asia, including China. What matters for your own programme is that the origin claim on the label matches the actual production route, and that fibre and care information follows the labelling rules of the market where the garment is sold.
What underwear is made in the USA?
Domestic United States production exists but covers a small share of the market, concentrated in premium and small-batch programmes using locally knitted cotton or performance fabric. Most mass-market underwear sold there is imported from Asia and Central America. The practical question for a buyer is labelling: fibre content, country of origin and care instructions must be substantiated before the garment ships, and the FTC textile labelling rules set how each appears. Decide the sourcing route first, then confirm the label wording matches it.
Whether you need a single sample or a repeat programme, start with the specification. Send the tech pack or reference, and Finetex Global will return costed options, minimums and a production calendar: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Men’s underwear manufacturer: garment types, fabrics and construction
- Capabilities: development, sampling, cutting, sewing and export documentation
- Quality control: bulk fabric testing, in-line checks and AQL 2.5 inspection
- Single factory or multiple suppliers: structuring a clothing supply chain
- Contact Finetex Global for a costed quotation
It sits inside the wider choosing an underwear manufacturer, where the rest of the sequence is set out.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day