
Wholesale Men’s T-Shirts: Blank Supply Chains and What Factory-Direct Actually Buys You
Wholesale T-shirt supply runs through blank brands, distributors and factories. Compare pricing tiers, availability, branding limits and reorder risk across all three.
Wholesale T-shirts reach a buyer through three routes: a blank brand, a distributor, or a factory. They look like variations on a price list, but they are different businesses with different strengths, and the right choice depends on whether you are buying availability, a dependable line of stock, or a product you intend to own. Comparing them on unit price alone produces the wrong decision most of the time.
What are the three supply routes?
Blank brand, distributor and factory.
A blank brand sells its own finished garments, a distributor resells stock from several producers, and a factory produces to your specification at volume.
| Route | Optimises for | Limitation |
|---|---|---|
| Blank brand | Consistent stock and known quality | No specification change |
| Distributor | Breadth and immediate availability | Least visibility on the source |
| Factory | Price at volume and full specification | Production lead time and minimums |
The three can coexist in one business, and often should: a distributor fills a gap in a fortnight, a blank brand provides a dependable line, and a factory builds the range that carries your name. What matters is knowing which role each plays, because the terms, the branding options and the reorder behaviour differ. Where a brand uses more than one, keeping the size chart consistent across them prevents customers from encountering the same nominal size described in two different ways.
It is also worth writing down which route each product line belongs to. A merchandise line sold to an existing audience and a signature range sold as a brand product have different requirements, and treating them the same usually means over-specifying one and under-specifying the other. The classification takes an afternoon and shapes every subsequent purchasing decision.
What does blank supply actually give you?
Consistency and speed, at the cost of specification.
Blank brands produce in volume and maintain stock across sizes and colours, so the product you validate in March is usually available in June and the quality varies little between orders.
That reliability is the product. A brand selling printed merchandise values it highly because the shirt is a substrate for artwork rather than a designed garment, and a print shop values it because the fabric surface behaves predictably across batches. Where the shirt itself is the product — its weight, its fit, its neck construction — blank supply cannot deliver, because those decisions were made by someone else for their own market. Ask what the composition and weight are, whether the same quality will be available next season, and what the size chart measures, then decide whether the answer describes the product you intend to sell.
When does factory-direct make sense?
When the garment itself is the product.
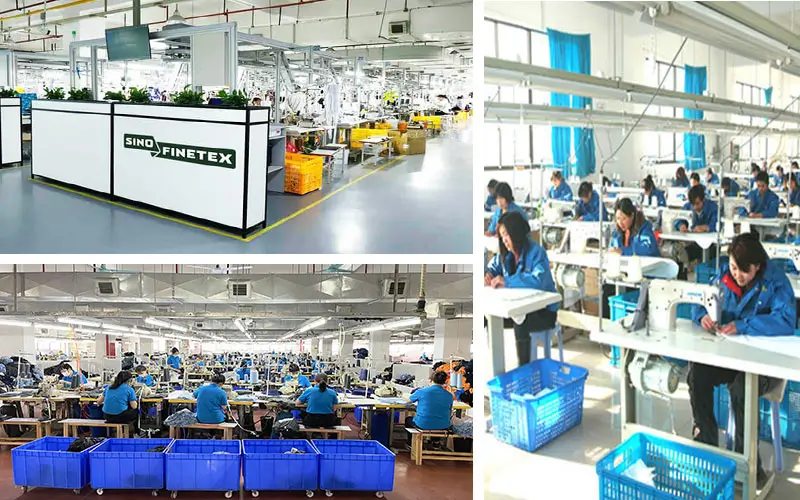
Factory production allows the fabric, the weight, the fit, the neck construction and the packaging to be specified, which is what makes a private label range different from a printed blank.
The economics work when volume is sufficient to absorb the setup and when the product will be reordered, because the tooling amortises across seasons rather than across one shipment. Before committing, ask what the difference in landed cost actually is at your volume, including sampling and any tooling, rather than comparing a factory unit price with a blank brand’s list price. Where the gap is small at your quantities, the specification may not be worth the additional lead time; where the gap is material and the product is intended to repeat, factory production is usually the better structure.
A practical way to test the decision is to price one style both ways at your expected first-year volume, including the reorder. Factory production usually looks more expensive on the first order and less expensive by the second, so the comparison should span both rather than stopping at the sample.
How do the price tiers differ between routes?
Blank brands publish; factories price by component.
A blank brand sells at list prices with volume discounts, while a factory prices the garment from its components: fabric, making, decoration, packing and the minimums each requires.
The practical consequence is that a factory quotation is negotiable through specification rather than through pressure. Asking what would have to change to reach the next price band usually produces a more useful answer than asking for a discount, because the components are visible. Where a supplier cannot explain what moves the price, the tier structure is probably arbitrary, which is itself worth knowing. For a brand comparing a blank brand with a factory, the useful comparison is landed cost at the same specification on the same size curve, not the two headline figures.
What are the branding limits of each route?
Blanks allow labels; factories allow the garment.
On blank supply you can add a neck label, a sleeve mark and packaging, while factory production allows the neck construction, the fit block and the fabric to carry your identity as well.
For resellers, the label and packaging route is often sufficient, and it costs nothing beyond artwork. For brands, the limitation appears when customers ask about the garment rather than the print: a shirt that feels different from what the weight suggests, or a neck that loosens after a month, cannot be corrected within a blank supply relationship. Where a brand intends to build a range, the branding ceiling is the reason to move to production rather than a reason to compromise. Where it intends to sell printed merchandise, blanks remain the sensible choice.
How should packaging and handling be compared?
By how the goods will actually move.
A blank brand usually ships in standard cartons with bulk or polybag packing, while a factory can produce retail-ready packing and label cartons to your specification.
Carton dimensions and weight determine how many shirts fit a pallet and what the freight costs per unit, so they belong in the comparison rather than in the warehouse. Ask both routes for the carton specification and the pack format, then calculate the landed cost including the handling you will have to do yourself. A blank order that arrives in bulk may require bagging and labelling in your warehouse, which is more expensive per unit than having the factory do it. That cost rarely appears in a price list and often decides the comparison.
How should size and colour curves be planned?
Weight the middle sizes and keep the colour count narrow.
Most T-shirt ranges sell the middle sizes several times faster than the extremes, and each colour adds a dye lot with its own minimum or stock risk.
On blank supply the constraint is stock: a colour that sells out may not return, so the curve should favour the sizes and shades that move fastest. On factory production the constraint is the lot, so the colour count determines the minimum more than the quantity does. In both cases the discipline is the same: a narrow range with a deep curve produces clearer sell-through data than a broad range spread thin. Ask what curve the supplier sees from comparable buyers, then adjust with your own sales rather than accepting a default. Where a supplier offers no view on the curve at all, the planning falls entirely to you, which is worth knowing before the order is placed.
Which questions reveal a reliable supplier?
Ask about specification, not price.
Five questions separate a supplier with a real product from one selling a listing, and each answer becomes part of the file you reuse on the next order.
- What is the composition and weight of the shirt you are quoting?
- Will the same quality and colour be available next season?
- What does the size chart measure, and how much tolerance applies?
- What pack format and carton dimensions will the order arrive in?
- Which stages of the production do you perform in-house?
These questions are easy for a supplier with a real product and difficult for one selling a listing.
Where a supplier cannot answer the first two, treat the product as a one-time purchase rather than the start of a range, and plan accordingly. The answers also build the file you will need for the next order: composition, weight, chart, packing and capability.
How should the decision be made?
On the role you need filled, then on landed cost.
Decide first whether you are buying availability, a dependable line of stock or a product you intend to own, and only then compare the costs of the routes that can deliver it.
That sequence prevents the most common mistake in this category, which is choosing a route for its price and discovering later that it cannot provide the specification, the branding or the reorder you assumed. Where a brand needs both immediate stock and a proprietary range, running two relationships deliberately is usually more effective than compromising with one. Keep the specification, the size chart and the label content consistent across both, so the customer experience stays coherent even when the supply chain is not.
FAQ
Who is the best bulk supplier for wholesale T-shirts?
It depends on what you need. A blank brand offers consistent stock and known quality, a distributor offers breadth and immediate availability, and a factory offers specification and price at volume. Ask each about reorder availability and the pack format before comparing unit prices, because those determine the landed cost.
Where can I find a bulk supplier of T-shirts?
Identify the role you need filled first, then approach suppliers who do that. For printed merchandise, a blank brand or distributor is usually the efficient route; for a branded range, a factory that can specify fabric, fit, neck and packaging is the right partner. Ask for the composition, weight and size chart in writing.
How do I get wholesale pricing on T-shirts?
Wholesale pricing follows volume and specification rather than negotiation. Ask what changes would move the order to the next tier, because it is often the colour count or the fabric choice rather than the quantity. A supplier that can explain the components of the price is working from a real cost model.
Is it cheaper to buy T-shirts from a factory or a distributor?
A factory is usually cheaper per unit at volume, but it carries a production lead time and minimums, and it only pays back if you reorder. A distributor is more expensive per unit but supplies immediately and in smaller quantities. Compare landed cost at the same specification rather than comparing list prices.
Next step for your team: tell the Finetex Global team whether you need stock, a dependable blank line or your own specification, and ask for the composition, size chart, pack format and reorder position on the products you are considering.
Sources: Supima — extra-long staple cotton; 16 CFR Part 303 textile labelling; U.S. Customs and Border Protection; OEKO-TEX STANDARD 100; ISO 9001 quality management.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day