
What are the best seamless bonding methods and adhesives: How to Read the Lists (and What They Leave Out)
A buyer sends a bonded undershirt for wash testing and it comes back with the hem tape lifting at the side seam. The sample looked right,…
A buyer sends a bonded undershirt for wash testing and it comes back with the hem tape lifting at the side seam. The sample looked right, the quotation looked normal, and the failure was designed in weeks earlier — in the adhesive an intermediary chose without seeing the fabric, or in a press temperature nobody recorded. Published lists of the best seamless bonding methods and adhesives rarely explain this, because they rank products while saying nothing about the machine, the dwell time, the pressure or the knit involved. This guide reads those lists for what they deliver, then sets out how to select, specify and verify a bonded programme in men’s knitwear, and where Finetex Global’s own position sits in that comparison.
The short answer on seamless bonding methods and adhesives
Seamless bonding joins knit edges with heat, pressure and an adhesive system rather than a stitch. In men’s knitwear, three routes hold up in production: ultrasonic welding, hot-melt film or tape bonding under a heat press, and taped seam sealing. Most programmes use a polyurethane film, with reactive or silicone adhesives for high-stretch waistbands and hems.
Undershirts and basics: where bonding does real work
On an undershirt, bonding earns its place where a stitch would show: the neckline, the sleeve hem and the bottom hem. A coverstitch on light single jersey reads as a ridge under a dress shirt, while a bonded or taped edge stays flat. On boxer briefs, the same logic applies at the waistband, where elastic application decides whether the band rolls or stays put.
That answer is deliberately narrower than the lists it responds to. Ranking adhesives by chemistry alone is like choosing a sewing thread without knowing the needle or the stitch. A bond is a system: fibre blend and fabric face, adhesive grade and weight, machine type, activation temperature, pressure, dwell time and cooling. Change one variable and the same film that held a nylon mesh hem will lift from a cotton-rich undershirt after a handful of home washes. The rest of this article separates the method from the adhesive, shows what each published route omits, and turns that into the tests, specification lines and quality gates that make a bonded programme repeatable on reorder.
Bonding means heat and pressure applied to a film or tape, so the fibre blend matters more than the adhesive’s marketing name. Cotton-rich surfaces absorb moisture and move slightly when pressed, while poly-rich knits behave more predictably. Weight compounds the effect: a heavier knit absorbs press heat more slowly, so settings that seal a light jersey can leave a thicker fabric under-bonded.
Undershirt weights in Finetex Global’s men’s knitwear range run from 120 to 220 gsm, and the order posture is 300 to 3,000 pieces per style, with stock fabric from 300 pieces and a custom knit or dye lot typically from 1,000 pieces per colour (indicative, subject to the latest quotation).
A practical note: run a bonded and a stitched version of the same style through one sample round, then wash and price both.
Seamless polos and T-shirts: where bonded construction earns its cost
For polos and T-shirts, bonding earns its cost in two places and rarely anywhere else: attaching a placket or collar without a bulky join, and finishing sleeve or bottom hems on lighter knits. Elsewhere, flatlock and coverstitch usually win, because the fabric tolerates them, the seam can be repaired, and the operators running them are not a bottleneck.
The technical constraint differs from bonding on trim. A bonded placket has to survive repeated buttoning, ironing and retail pressing, and a tape that creeps under heat shows up as a wavy placket after the first wash. Ultrasonic welding suits poly-rich jersey, where the fibre itself can fuse; hot-melt film suits blends that need an intermediate layer.
Polo and T-shirt weights sit in the 140 to 220 gsm band in the Finetex Global range, heavy enough to resist adhesive strike-through but slow enough to press that bond length drives cycle time.
A practical note: put the bonded edge position, finished width and seam allowance on the tech pack as a dimensioned drawing, then confirm that the bonded edges connect to the men’s underwear and basics programmes without introducing a second size chart.
Reading a published bonding and adhesive list: what the entries leave out
A published list of bonding adhesives tells you what a product can do in a laboratory; it rarely tells you whether your fabric will accept it. Use those lists for chemistry, then rebuild the entry around your own garment, machine and care label. The table below sets the common routes side by side on the variables that decide a first order rather than a supplier’s data sheet.
| Bonding route | How the bond is formed | Where it fits in men’s knitwear | What a published list usually omits | What to verify before ordering |
|---|---|---|---|---|
| Ultrasonic welding | High-frequency vibration and pressure soften thermoplastic fibre or a thermoplastic film at the interface so the plies fuse, without a stitched seam | Poly-rich jersey and mesh; undershirt hems, sleeve openings, light T-shirt edges | Horn and anvil geometry, weld width and cycle time, and whether the fibre is weldable at all | Whether the fabric can fuse, and how the weld behaves after the care cycle printed on the label |
| Hot-melt film bonding | A polyurethane or thermoplastic film sits between the plies and is activated by temperature, pressure and dwell time, then holds as it cools | Bonded necklines, plackets, folded hems and bonded waistbands across knit blends | Activation window, pressure, dwell time, film weight per square metre and cooling time | The grade and lot of the film, plus the press settings used to make the approved sample |
| Seam-sealing tape | A coated tape is applied over a stitched or folded seam to seal and reinforce it | Performance tees and compression-oriented knitwear where a seam takes abrasion or moisture | Tape width and elasticity relative to the seam it covers, and whether stitching is still required underneath | That the tape stretches with the garment instead of restricting its recovery |
| Reactive (thermosetting) adhesive | A cross-linking adhesive cures into a durable flexible bond rather than cooling into one | Stretch zones and constructions where press temperature is limited by the fabric | Cure time, humidity and the working life of a mixed adhesive | Whether the cure schedule fits the production flow, and how the bond holds after repeated laundering |
| Silicone or elastic adhesive deposition | An elastic adhesive is applied in a pattern of lines, dots or a mesh, then cured in place | Waistbands, hems and panels that must stay flat while stretching with the body | Pattern density, deposit weight and the substrate’s surface energy | Recovery after stretch, and whether the deposit stays flexible in cold conditions |
| High-frequency (dielectric) welding | An alternating field heats polar material internally, welding thick or coated substrates from the inside out | Coated and technical constructions, generally outside standard knit programmes | Material polarity requirements, tooling cost and edge quality | Whether the fabric carries enough polar material for the process, and what the tooling costs to build |
The same caution applies outside men’s knitwear: lace, women’s lingerie and coated technical shells are bonded too, but those categories sit outside Finetex Global’s men’s knitwear scope and are treated here as criteria to evaluate elsewhere rather than as a claimed capability. Finetex Global’s own position in this comparison is disclosed: it is a Shenzhen OEM and ODM manufacturer of men’s knitwear, the operation behind Finetex Textile Co., Ltd., and not an adhesive supplier, so the metrics applied above are mechanism, substrate fit and verifiability, applied identically to every route.
OEM and ODM requests: what to lock so a bond reproduces
A bonded programme more often fails at reorder than at first order, because the adhesive grade, the film lot and the press settings were never written into the specification. Lock them while the approved sample is still on the table; chemistry chosen by a name that sounds compatible is the usual cause of a second batch that behaves differently.
A version-controlled specification should carry the adhesive chemistry and grade, the film or tape width, the bond position on the pattern, the machine type, and the activation temperature, pressure and dwell time used to make the sealed sample. The approved physical sample, signed and held by both parties, is the reference against which bulk is measured; a photograph of a seam is not a substitute.
Where a brand supplies its own adhesive, compatibility cannot be confirmed until a trial is run, which moves cost into sampling. Where the factory sources the film, the same grade has to remain available at reorder.
A practical note: ask in writing what happens when a specified film is discontinued, and confirm that any replacement is re-tested on the garment, because fibre content, care instructions and country-of-origin labelling have to stay accurate after a construction change.
High-tech seamless T-shirts: which performance claims a bond can carry
A bonded seam can carry a comfort claim and a recovery claim; it cannot carry a moisture or durability claim on its own. Removing stitch bulk supports statements about smoothness and reduced abrasion, and those can be demonstrated on a finished garment. Claims about wicking rate, stretch recovery or wash durability still need test reports on the garment as sold, not on the adhesive as delivered.
Adhesives also add chemistry to a product that touches skin, so restricted-substance coverage belongs in the order file before any claim is published. Finetex Global holds OEKO-TEX Standard 100, renewed annually, and runs buyer-specific testing through laboratories including SGS. Composition and care statements follow the same discipline: fibre content and country of origin are regulated under the US Textile and Wool Acts and 16 CFR Part 303, while care symbols for the export market follow GINETEX conventions.
A practical note: a bonded garment’s care instructions can differ from those of a stitched equivalent, so confirm the label wording with the bond that was actually tested rather than reusing the previous season’s label.
FAQ
What’s the best bonding adhesive?
There is no single adhesive that wins across a range, because the answer depends on the fibre blend, the stretch the seam has to follow, the bond width and the care conditions on the label. In practice, a polyurethane hot-melt film covers most men’s knitwear bonding, reactive types suit constructions that cannot take high press heat, and elastic or silicone adhesives suit stretch zones such as waistbands. The honest test is not the data sheet but a finished garment washed on the cycle your label claims, with the film grade and process settings recorded.
Which bonding adhesive is the strongest?
Strength is a property of the joint, not of the adhesive family alone. Peel and shear behaviour change with bond width, fabric surface, pressure, dwell time and cooling, so a well-matched film applied across a wider bond usually outperforms a higher-specification adhesive applied badly. Ask the supplier for performance data on your fabric combination rather than on a generic substrate, then compare bonded samples that have been through the same wash cycle. A bond that holds through laundering and wear is doing more for the programme than one that only wins on a bench test.
What are the six types of adhesives?
The classification most adhesive suppliers publish runs to six families: water-based, solvent-based, hot-melt, reactive, pressure-sensitive and radiation-curing. Only two of those carry most apparel bonding: hot-melt, which covers the films and tapes activated on a press, and reactive types, which cure rather than cool. Pressure-sensitive chemistry appears in tapes and labels rather than in structural seams, while solvent-based products raise restricted-substance questions on skin-contact garments. Knowing the six families is useful for reading a specification sheet; it does not tell you which route suits your seam, which is a fabric and tooling question.
What is the fastest bonding construction adhesive available?
Speed in a factory is usually cycle time, not curing chemistry. A thermoplastic hot-melt film activated on a platen press cycles faster than a reactive adhesive that needs cure time, and where the knit is poly-rich, ultrasonic welding fuses the fibre itself with no consumable layer at all. The fastest option is only usable if the fabric tolerates the temperature and the finished bond passes the wash test, and a fast cycle that scorches a cotton-rich face is not fast once the batch is re-made. Let the material set the speed.
Selection by programme type: value, premium, sport and eco
Match the bonding route to the programme rather than to the season’s trend. A value line is served by stitched seams with bonding used only where stitch bulk would show, built on stock fabric so the entry point stays at 300 pieces per style. A premium line justifies a fine-gauge bonded finish and a custom knit or dye lot, which typically starts at 1,000 pieces per colour. Sport programmes are specified around recovery, so elastic adhesive or tape in stretch zones matters more than surface smoothness. Eco-led programmes add documentation, because the adhesive joins the restricted-substance and traceability story rather than staying a hidden trim.
The trade-off is arithmetic. Each step up adds a bonded operation, a consumable and a press cycle, and all three scale with bond length rather than with garment count. That programme logic follows the decision path set out in choosing a men’s underwear manufacturer by programme.
A practical note: decide the programme type before requesting quotations, because the same brief sent as a value enquiry and as a premium enquiry returns specifications that cannot be compared line for line.
Cost and MOQ anatomy: where the bond sits in the unit price
Fabric dominates the unit cost at roughly 45 to 60 percent, but bonding appears in two less obvious lines: the film or tape as a consumable trim, and press or welding time as labour. Both scale with bond length and cycle time, so a heavily bonded style carries a higher break-even volume than a stitched one.
A costed quotation should show fabric, labour, trim and packing separately, with the adhesive identifiable inside trim, so a substitution can be judged on its full effect. Minimum order quantity is a tooling and colour decision: stock fabric keeps the entry point low, a custom colourway commits a dye lot, and a new bonded construction adds a trial.
Finetex Global quotes 300 to 3,000 pieces per style, with stock fabric from 300 pieces and a custom knit or dye lot typically from 1,000 pieces per colour; quotations issue within one working day, are held for 90 days, and sample charges are credited against the bulk order. Those figures are indicative and subject to the latest quotation.
A practical note: compare quotations on identical bond lengths and film widths, because a shorter tape run looks cheaper without being cheaper.
Pre-production tests and QC gates for a bonded programme
Add two bonding-specific checks to a standard knitwear quality plan: a bond performance check on the sealed pre-production sample, and a wash test on the finished garment. Everything else is the same discipline that prevents shade and size drift, and skipping it multiplies a single bad press setting across the whole grade.
Upstream, bulk fabric is inspected for shade continuity, shrinkage, weight per square metre and colour fastness before cutting, because an adhesive cannot rescue a fabric that moves. During the run, in-line checks at 30 percent and 70 percent catch a drifting press or a changing film lot while the run can still be corrected. Final inspection is AQL 2.5 with a photo report before packing and shipment, which is the same gate Finetex Global applies to men’s knitwear orders, and the bonded construction is verified under the quality control process rather than as a separate standard.
A practical note: agree the peel or tensile value and the wash cycle with the buyer before bulk, and record the result on the sample that was pressed with production parameters; a sealed bonded control sample in the order file turns a later dispute into a measurement.
From sample to bulk: the working sequence for a bonded programme
A bonded programme runs through the same three gates as any knitwear order — sample, specification lock, bulk — with one addition: the press parameters travel with the specification. Sampling establishes fit and hand, the locked specification freezes fibre, weight, elastane content, adhesive grade and bond geometry, and production runs against that frozen version.
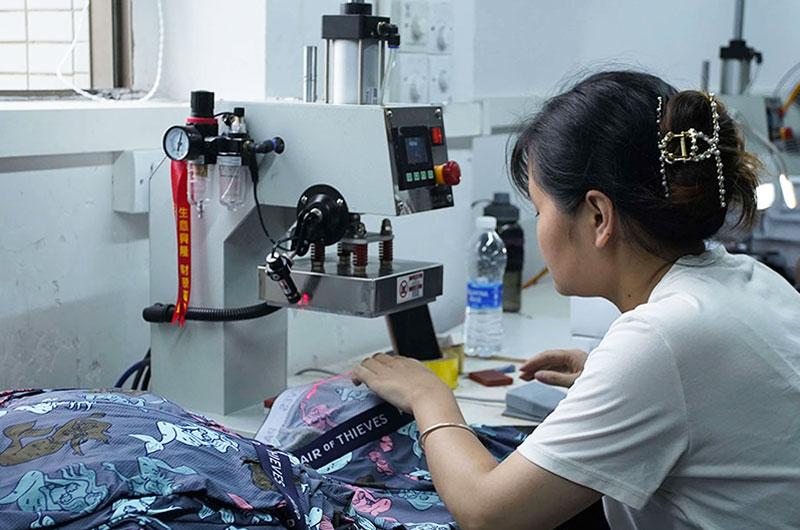
Finetex Global works with a fit and development sample in about five to seven working days and a graded size set in about ten to twelve working days; these timings are indicative and subject to the latest quotation. Once the physical sample is approved, patterns are graded once and locked, one named merchandiser carries the order, and updates are issued in writing each week. Starting with apparel design and development before the first pattern is cut keeps the bonded edges and the size chart aligned.
Ask for a costed second opinion before you place the order. Finetex Global will read your specification, flag the cost lines that move the price and confirm what the fabric minimum per colour would be: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Choosing a men’s underwear manufacturer in China by programme
- Men’s underwear and basics manufacturing programmes
- Boxer briefs factory capabilities and fabric options
- Apparel design and product development support
- Quality control gates for knitwear production
For the surrounding decisions in the same programme, see the the apparel fabric selection guide.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day