
How do bonded seams create a seamless look in techwear: A Manufacturer’s Walkthrough
Your bonded tape sample came back from the wash test with a lifted edge, bulk fabric is already booked for three weeks, and the launch date…
Your bonded tape sample came back from the wash test with a lifted edge, bulk fabric is already booked for three weeks, and the launch date has not moved. Bonded construction fails quietly in exactly that way: the seam looks clean on the table and separates on the fourth domestic wash. This walkthrough is written from a men’s knitwear factory floor rather than a marketing deck — the bonding routes, fabric limits, cost structure and QC gates that decide whether a bonded seam survives a retail programme. Finetex Global (legal entity Finetex Textile Co., Ltd.) has manufactured men’s knitwear for export from Shenzhen since 2004, so the sections below use our own programme experience where relevant and mark every figure as indicative and subject to the latest quotation.
The short answer
Bonded seams create a seamless look because they join fabric with heat, pressure and an adhesive film instead of thread, so there is no stitch line, no needle hole and no raised seam allowance to break the surface. The result is a flat, continuous panel edge that stretches with the knit.
How Does a Bonded Seam Differ from a Traditional Stitched Seam?
A stitched seam holds a garment together with thread; a bonded seam holds it together with polymer. That difference drives the flat appearance, the absence of needle holes, the tooling cost and the way the join behaves under repeated extension. In a stitched construction the needle punctures the knit, the allowance is folded inside or pressed flat, and the join is only as elastic as the stitch class and thread allow. Flatlock and cover-stitch remain right for most men’s underwear, T-shirts and sweatshirts.
That single mechanism explains both the appeal and the risk. Because nothing punctures the knit, a bonded edge on a boxer brief leg opening, a seamless polo hem or a compression panel reads as one continuous surface rather than a join, and there is no perforation for moisture to wick through. Because nothing is stitched, the join has no mechanical redundancy: if the adhesive parameters drift, the seam has no thread to fall back on. Everything practical about bonding — fabric selection, tooling cost, testing and care labelling — follows from that trade. The sections below cover stitched comparison, bonding methods, fabric fit, durability, procurement choice, cost, QC and the sampling sequence.
Bonding removes the thread path entirely. A thermoplastic adhesive film sits between two fabric surfaces, and heat and pressure — or high-frequency energy — melt it into the fibre surface, so the join is held by adhesion plus mechanical keying into the knit structure, with no needle hole to open under stretch. The trade-off is process control: bond strength depends on temperature, dwell time, pressure and film grade, all locked to a fabric lot. As an indicative starting point we allow 5–7 working days for a development sample, subject to the latest quotation, and a first bonded construction often needs a second tooling pass before parameters are stable.
| Variable | Stitched seam (flatlock or cover-stitch) | Bonded seam |
|---|---|---|
| Joining medium | Thread and needle | Adhesive film or tape plus heat, pressure or high-frequency energy |
| Surface profile | Visible stitch line; allowance adds bulk | Flat, continuous panel with no needle holes |
| Stretch and recovery | Governed by stitch class, thread and elastane content | Governed by film grade; a stiff film limits stretch |
| Moisture and wind path | Needle perforations can wick | Unperforated join, no wicking path at the seam |
| Tooling and setup | Machine settings plus a seam guide | Bonding press, die or roller, film grade and a locked parameter card |
| Rework | Unpicked and re-sewn | Usually re-cut; the bonded panel is a consumable |
| Wash tolerance | Tolerant of higher wash temperatures | Set by the film and fabric combination |
What Are the Primary Methods for Creating Bonded Seams?
Four bonding routes reach volume production in men’s knitwear: hot-melt tape, ultrasonic, high-frequency welding, and edge bonding. The choice follows fibre content, panel geometry, order volume and the stretch the seam must deliver, not machine availability, and most knit programmes run hot-melt tape bonding, whose film grades span enough hardness and elongation for common knit blends.
Hot-melt tape bonding presses a pre-cut adhesive film between two surfaces under controlled heat, dwell and pressure. Ultrasonic bonding melts the thermoplastic content at the interface with high-frequency vibration, removing the tape and its bulk — a fit for synthetic-rich sportswear and compression panels. High-frequency welding is reserved for heavier synthetic stacks. Edge bonding secures a turned or folded cut edge with a narrow tape, giving a clean hem without a fold line.
Two constraints matter. Ultrasonic and high-frequency routes need a minimum thermoplastic content, so a bamboo-rich or 100% cotton knit is normally tape-bonded rather than welded. Every route also needs order-specific tooling, so at MOQ from 300 pieces per style on stock fabric, bonding should be judged against flatlock on total cost, not appearance alone (indicative, subject to the latest quotation).
Which Fabric Types and Garment Categories Benefit Most?
Bonding earns its cost where a flat, unpunctured surface is the product promise: men’s underwear such as boxer briefs, trunks and briefs, seamless tees and polos, compression and sportswear, and loungewear where a soft hand-feel at the waist matters. It fits poorly on heavy builds — 420 gsm French terry or 500 gsm brushed fleece — where loft makes adhesion hard to hold across a lot, and on programmes washed hot.
Synthetic and elastane-rich knits accept ultrasonic energy and low-temperature films readily. Modal, micro modal, bamboo viscose and lyocell bond well with tape but need tighter moisture control, because a small moisture swing changes the heat the film needs to reach bonding temperature. Cotton-rich knits handle well but usually need a higher-melt film and a longer dwell. Lighter 120–180 gsm jersey and interlock bond consistently; heavyweight fleece is better served by flatlock.
Garment category then dictates where the bond goes. Bonded edges suit leg openings, necklines and hems, where the consumer touches the surface; bonded structural joins suit side panels on compression garments. On a boxer brief, bonding the leg opening while flatlocking the rise is a common, economical split.
What Are the Key Advantages and Potential Limitations?
The commercial advantage of bonding is specification, not decoration. A flat join reduces bulk under a fitted garment, so a boxer brief or compression top disappears under trousers in a way a raised stitched allowance does not. Removing the needle removes the perforation path, which lifts moisture and wind resistance at the seam and reduces chafe on a moving panel. Bonding also removes the stitch-density variables that produce wavy seams on elastane-rich knits.
The limitations deserve to be costed before the decision. Adhesive films and tapes are consumables with their own unit cost, quoted separately from fabric and labour. Bond strength is sensitive to parameter drift, so bonding lines need locked parameter cards and frequent verification. Repair is poor: a lifted bonded edge is normally re-cut rather than re-sewn, which raises the cost of rework across a graded size set.
One scope boundary is worth stating plainly. Bonded and taped construction is central to technical outerwear — hardshell jackets and taped waterproof shells — and that category sits outside men’s knitwear. Where a programme needs those constructions, treat this article as evaluation criteria and verification method rather than a claim of factory capability.
How Does the Durability and Care Compare to a Stitched Seam?
On a well-controlled programme, a bonded seam matches or beats a stitched seam in its two weakest areas: resistance to needle-hole wicking and resistance to bulk-driven abrasion. Heat tolerance is the exception — thread survives boiling, while adhesive films have a softening range, and above it the join creeps. The care label, not the seam appearance, is the controlling document for a bonded programme.
Durability is handled as measurable checks rather than a claim. Our bulk fabric inspection covers shade continuity, shrinkage, weight per square metre and colour fastness; a bonded programme adds peel and shear strength, elongation and recovery after repeated extension, and delamination after wash cycles to the label instructions. Where a retailer requires third-party verification, testing is arranged through SGS or another nominated laboratory.
Care instructions should be written by the film and fabric combination, not by habit. Disclosure and care symbols follow the destination market: the FTC textile labelling guidance and 16 CFR 303 for the United States, and GINETEX care symbols where the market follows that system. Publishing a hot wash out of habit can fail a bonded seam that would have passed cooler.
How to Choose by Programme Type: Value, Premium, Sport and Eco Lines
Bonding is not a quality tier; it is a construction decision that should follow the programme’s price point and use case. A value multipack, a premium single-piece programme, a performance line and a certified-fibre eco line place their money in different places, and the construction choice should reflect that. Specifying bonding on a price-driven multipack usually moves cost without moving perceived value, while specifying flatlock on a premium fitted piece often leaves visibility where the brief promised a clean surface.
The pattern below is how we frame the decision in a quotation conversation. Value programmes put cost into the multipack economics and the waistband; premium programmes put it into the surface, the hand-feel and the bonded finish; sport programmes put it into stretch, recovery and chafe reduction, where bonding and flatlock are frequently combined; eco programmes put it into certified fibre and traceable claims, where the adhesive film’s own documentation matters as much as the fabric certificate.
| Programme type | Construction emphasis | Where the money sits | Main risk to control |
|---|---|---|---|
| Value multipack | Flatlock or cover-stitch body, elastic waistband, minimal bonded edges | Fabric yield, waistband elastic, packing | Shade continuity and size consistency across a multipack |
| Premium fitted | Bonded leg openings and hems, flatlock structural joins | Fabric quality, bonded finish, low volume tooling | Whether the bonded finish justifies the tooling cost at the order volume |
| Sport and compression | Bonded or ultrasonic side panels, flatlock at high-stretch joins | Performance blend, elastane content, film grade | Recovery retention and delamination after repeated extension |
| Certified eco | Construction chosen for the fibre; bonded only where the film is documented | Certified fibre, chain-of-custody paperwork, testing | Claims that the fibre and the adhesive cannot both support |
Cost and MOQ Structure: Where 45–60% of Unit Cost Sits
Fabric typically accounts for roughly 45–60% of unit cost, with labour, trim, adhesive consumables and packing making up the rest. Bonding shifts that structure rather than raising it: sewing minutes fall, the consumable line rises, and tooling becomes a fixed cost absorbed by order volume — dominant per unit on a 300-piece run, faded by 3,000.
Two levers do most of the work. Heavier fabric raises cost and can reduce bond reliability on lofted surfaces, so weight added for perceived quality can work against the seam. Higher elastane content improves recovery but raises fabric cost and narrows the process window, because elastane-rich knits move under heat. The answer is usually a moderate elastane percentage matched to an elongation-tested film.
MOQ follows the same logic. Stock fabric can start at 300 pieces per style in mixed sizes; a fully custom knit or dye lot typically starts at 1,000 pieces per colour, and about a third of our programmes start below 1,000 pieces per style. Quotations show fabric, labour, trim and packing separately, sample charges are credited against bulk, and pricing is held 90 days — all indicative, subject to the latest quotation.
Pre-Production Tests and QC Gates for a Bonded Programme
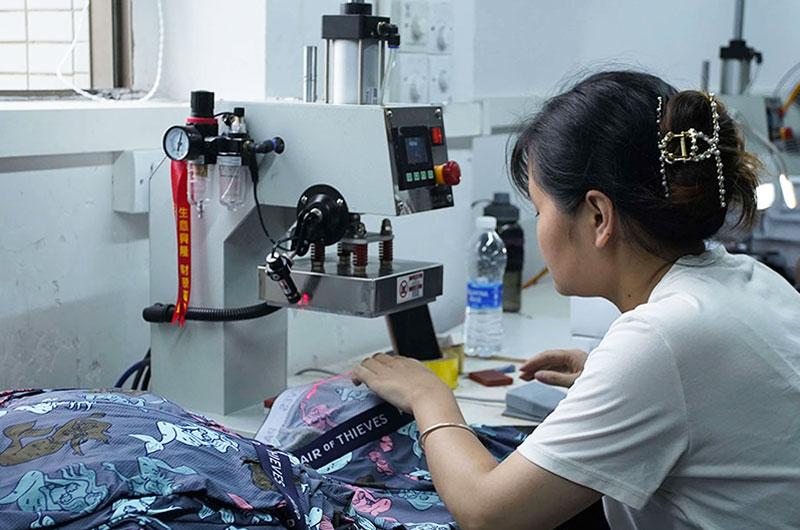
A bonded programme needs its own verification gates, because a pass on the fabric does not mean a pass on the join. Our sequence starts before cutting and continues through packing, with each gate producing a record that travels with the order. Where a retailer specifies a test package, that package governs.
Before cutting, bulk fabric is checked for shade continuity, shrinkage, weight per square metre and colour fastness. Production then runs with in-line QC at roughly 30% and 70% of the run, which is where a drifting bonding temperature or a misaligned tape shows up early enough to correct. Final inspection follows AQL 2.5 with a photo report issued before packing and shipment.
A bonded programme adds lot-level peel and shear checks, elongation and recovery measurement after repeated extension, and a wash trial to the care instruction that will appear on the label. Compliance documents are assembled before claims are published: OEKO-TEX Standard 100 is renewed annually with certificates held in the order file, alongside fibre composition and chain-of-custody documents for bamboo, Lenzing modal, TENCEL and recycled polyester where those fibres are used.
How to Start: Sampling, Specification Lock and Bulk
The fastest way to de-risk a bonded programme is to separate the appearance decision from the durability decision. Approve the look on a development sample, then approve the bond on tested production fabric, because a sample built from a substitute fabric can pass visually and fail in bulk. Our standard sequence runs a fit and development sample in 5–7 working days and a graded size set in 10–12 working days, subject to the latest quotation.
Specification lock is the step buyers most often skip. Once the sample is approved, we hold a version-controlled specification and an approved physical sample on both sides, so the bonding parameter card, film grade, fabric lot and measurement chart are fixed against a single reference. That discipline is how shade differences, half-size deviations and seam drift get caught before they become thousands of rejected pieces.
From there the programme moves into bulk production with one named merchandiser, weekly written updates and export documentation under the same production plan. If you are comparing suppliers at this stage, the apples-to-apples method for comparing factory quotations shows what to normalise, and the quality control process explains the inspection gates above.
FAQ
What are the 7 different types of seams?
Seven seam types are commonly taught in garment construction: plain or superimposed, French, flat-felled, lapped, welt, edge-stitched or top-stitched, and bound. Published seam-classification systems group the same constructions by class and code rather than by nickname, so a tech pack is safer when it carries a construction drawing and code instead of a name alone. Bonded and welded joins sit outside that list entirely, because no thread and no needle are used at the join.
Do seamless shirts exist?
True zero-seam shirts exist only as tube bodies. Circular-knit machines can produce a continuous tubular body with no side seams, which is how seamless tees, polos and undershirts are made. Shoulders, neckline, sleeve joins and hems still have to be joined or finished, so “seamless” describes the body panel rather than the whole garment. Those remaining joins are where flatlock or bonded tape is used, which is why the surface looks continuous even though the garment is not literally join-free.
How do they make shirts with no seams?
A circular-knit machine knits a tube to the finished body circumference, so the torso needs no side seam; the neckline, armholes and hem are then finished on the machine or joined with a flat, low-profile construction. Where a bonded finish is specified, adhesive film or tape replaces thread at those joins, and the parameter card — temperature, dwell, pressure and film grade — is locked to the production fabric lot. Sampling for such a programme is indicative at 5–7 working days for a development sample, subject to the latest quotation.
If you want the specification reviewed against your own target price, send the tech pack, reference sample or competitor garment. Finetex Global returns a costed quotation and sampling timeline, with all figures subject to the latest quotation: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Men’s underwear manufacturing programmes
- Boxer brief and trunk development at our Shenzhen factory
- Apparel design and product development support
- Quality control and inspection gates
- How to compare clothing factory quotes on an apples-to-apples basis
This page is part of our the apparel fabric selection guide, which covers the decisions before and after it.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day