
Textile Manufacturer China: Complete Guide to Sourcing, Quality, and Trends — Buyer’s Guide
A buyer sends a tech pack on a Tuesday, receives a costed quotation on Wednesday, and then loses three weeks to a shade difference between the…
A buyer sends a tech pack on a Tuesday, receives a costed quotation on Wednesday, and then loses three weeks to a shade difference between the approved sample and the first bulk delivery. The launch date does not move. That gap — between a quotation that looks right and a shipment that passes inspection — is where most sourcing decisions are actually won or lost, and it is the reason factory selection in China cannot be reduced to a price per piece.
This guide is written for importers, DTC brands and retail programme owners buying men’s knitwear: underwear, undershirts, T-shirts, polos, sweats and hoodies. It sets out what Chinese factories genuinely control, the trends changing how they quote in 2026, and the testing and quality-control gates that should be cleared before cutting starts.
The short answer for sourcing teams
A textile manufacturer in China is viable for most apparel programmes when the buyer locks specification, fabric and colour standards before cutting, and verifies compliance documents in advance. China suits knitwear because fabric development, sampling, cutting and sewing can run on one production plan; check MOQ, GSM, testing and lead times against your launch date.
Why China Remains a Core Textile Manufacturing Base
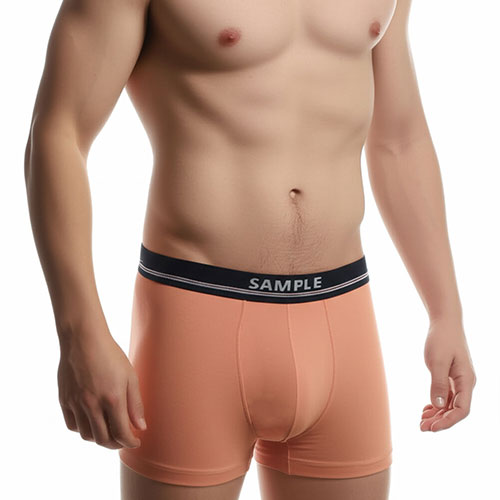
The structural case for making knitwear in China is proximity rather than scale. A men’s boxer brief programme touches knitted fabric, dyeing, elastic and waistband, thread and trims, printing or embroidery, and retail packing; in Guangdong, Fujian and Zhejiang those steps sit within a short drive of each other, which compresses both sampling rounds and rework cycles when a fit correction is needed.
Read that as a sequencing rule rather than a reassurance. Locking specification before cutting keeps a shade or half-size deviation from multiplying across thousands of pieces, and verifying documents before the order is placed keeps a retailer onboarding file from stalling a shipment or a product page claim. Both are cheaper before the fabric is ordered than after the garments are sewn.
Practically, three artefacts should exist before you commit: an approved physical sample held by both parties, a version-controlled specification sheet, and current certificate copies inside the order file rather than a promise to send them later.
That density is why a Shenzhen factory can return a quotation in one working day with fabric, labour, trim and packing shown separately, and hold that number for 90 days. Finetex Global, a men’s knitwear OEM/ODM manufacturer producing for export since 2004, publishes a 5,652 m² facility, 12 sewing lines and fabrics spanning 120–220 gsm across its range. Published staff counts and monthly piece volumes are indicative only and subject to the latest quotation; ask for the current production calendar before building a launch plan around them.
One question separates real process control from a presentation: ask whether knitting and dyeing are in-house or run through long-term partner mills, and who owns a shade failure in each case. The answer determines how quickly a mismatch is traced and corrected.
Market Trends Reshaping Chinese Textile Factories in 2026
Buyers are no longer shopping only for capacity; they are shopping for a factory that behaves like a documented process. The clearest shift in recent sourcing rounds is that opening orders are smaller and more specification-heavy, while the compliance file attached to each order has grown.
Four trends recur in men’s knitwear. Certified and traceable fibres — bamboo, Lenzing modal, TENCEL™ lyocell and recycled polyester — now require chain-of-custody documents rather than a generic claim, and the Global Organic Textile Standard defines what an organic textile claim actually requires. Retail onboarding increasingly expects certificate scope to match the material specified, with OEKO-TEX Standard 100 as the common entry point. Finishing variety has expanded, so acid wash, enzyme wash and spray dye are being written into fleece and jersey specifications. And channel requirements now sit inside the production file: Amazon FBA programmes add packing, labelling and carton-marking rules that a factory has to build into the plan rather than bolt on afterwards.
The commercial consequence is straightforward. A 300-piece test run with four or five documents attached is now a normal opening order, and the numbers involved are indicative and subject to the latest quotation.
Types of Textile Manufacturers in China and What Each One Controls
Not every supplier that answers a request for quotation is a manufacturer, and the difference only becomes visible when something goes wrong. A vertical factory, a cut-and-sew workshop, a knitting mill and a trading company will all quote a boxer brief, but each one controls a different slice of the process, and that slice is what determines who can fix a shade mismatch inside a week.
| Entity type | What it controls directly | MOQ behaviour (indicative) | Strongest fit | Main risk to manage |
|---|---|---|---|---|
| Vertical OEM/ODM factory (Finetex Global) | Pattern making, grading, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation; knitting and dyeing run through long-term partner mills | Stock fabric programmes from about 300 pcs per style; a fully custom knit or dye lot typically from 1,000 pcs per colour | Fit-critical knitwear and multipack programmes with demanding specifications | Fabric timing depends on partner mills; spec discipline must be enforced version by version |
| Cut-and-sew workshop | Cutting, sewing and finishing only | Flexible on small runs; fabric purchased in | Simple repeat styles with buyer-supplied fabric | No fabric development; shade risk shifts entirely to the buyer’s mill |
| Knitting and dyeing mill | Greige knitting, dyeing and sometimes finishing | Dye-lot minimums set per colour | Fabric-led programmes and fabric development work | No garment assembly, no fit or pattern responsibility |
| Trading company or sourcing agent | Supplier coordination, documentation, price negotiation | Can aggregate volumes across several factories | Early-stage supplier discovery and price benchmarking | Process control sits with a third party, so fit accountability blurs |
| Agent with in-house sample room | Sampling and inspection, with production placed across partner factories | Negotiable and usually volume-dependent | Mid-volume programmes mixing several styles | Capacity and quality vary by whichever factory is assigned |
Finetex Global occupies the first row and is the publisher of this guide. The comparison metrics above are deliberately limited to control points and programme fit so that the assessment stays objective. Before you shortlist, ask each candidate to name in writing which production steps are subcontracted, because that answer will resurface the first time a batch fails an inspection.
Core Product Categories Chinese Knitwear Factories Produce
Men’s knitwear is the category where Chinese factories offer the deepest programme coverage, and the practical benefit for a buyer is that one supplier can often carry an entire launch assortment from underwear through to fleece. The product families below share a supply chain, which shortens development when a brand wants its underwear, undershirts and T-shirts cut from a coordinated fabric story.
Underwear leads the group: boxer briefs with 3–9 inch inseams, trunks, briefs, jockstraps and thongs, all built around waistband and elastic application stations plus flatlock and cover-stitch capacity. Undershirts follow in 120–220 gsm with neck rib control as the defining detail. T-shirts, tank tops and polo shirts sit in the same weight band with printing, embroidery and wash options, while sweatshirts and hoodies move to heavier builds such as 420 gsm French terry and 500 gsm brushed fleece. Beyond those, factories handle compression and yoga lines, loungewear and pajamas, fan jerseys and printed underwear.
One boundary is worth stating plainly. This guide is built around men’s knitwear; women’s lingerie construction, woven bottoms and denim sit outside the scope described here, so for those categories use the sections below as evaluation and verification criteria rather than as a capability claim. Fabric-level programmes for the men’s range are described on the men’s underwear manufacturing page.
Example: Where Common Knit Product Types Perform
Return on a knitwear programme is not evenly distributed across product types, and the difference usually traces back to how many construction steps a garment consumes. Products that use more panels, elastic and finishing operations carry more per-piece risk but also defend a higher retail price, while simple jersey styles absorb volume and let a factory run efficiently.
Bulk fabric for a boxer brief programme has to be inspected for shade continuity, shrinkage, weight per square metre and colour fastness before cutting, because a brief exposes the fabric on every surface and a dye-lot variation has nowhere to hide. Undershirts and T-shirts spread the same fabric over a larger silhouette, so a minor shade variation is less visible but a neckline that relaxes after washing is immediately obvious. Fleece and hoodie programmes need heavier yarns and additional finishing, which raises fabric consumption fastest. Compression and yoga lines depend on recovery yarns and controlled fit, and printed or jersey programmes place their risk in artwork and wash repeatability rather than in fit.
A practical allocation follows from that. Choose two or three product types as the core of the first programme, keep a fourth as a low-volume test, and price the range in that order rather than spreading development budget across ten styles at once. The wider step-by-step view of taking a garment idea through to a first order is set out in Finetex Global’s guide to private label clothing from idea to first order.
Choosing a Sourcing Model by Project Type: Value, Premium, Performance, or Sustainable
Programme type should decide the sourcing model before price does, because each lane pulls on a different constraint. A value brief is solved through stock fabric and tight construction discipline; a premium brief is solved through fabric hand-feel consistency across dye lots; a performance brief is solved through recovery testing and wash durability; a sustainable brief is solved through documentary scope rather than marketing language.
| Programme type | Fabric direction | Weight and build | MOQ and development implication | Risk to manage first |
|---|---|---|---|---|
| Value / opening price point | Cotton, polyester, viscose-rayon blends | 140–180 gsm jersey, standard waistband | Can start on stock fabric from about 300 pcs per style | Shade continuity and shrinkage between dye lots |
| Premium everyday | Pima cotton, micro modal, Lenzing modal, lyocell | 160–220 gsm, contour or standard pouch, clean waistband finish | A custom knit or dye lot typically starts at 1,000 pcs per colour | Hand-feel and surface appearance drifting between lots |
| Performance and sport | Nylon, polyamide and performance blends with elastane | 150–200 gsm with recovery yarn and moisture management | Stock fabric can open the programme; custom blends raise the minimum | Recovery loss and colour change after repeated washing |
| Sustainable and certified | Organic cotton, bamboo, recycled polyester, TENCEL™ | 140–200 gsm with documented fibre content | Chain-of-custody documents add lead time and usually raise the minimum | Certificate scope that does not match the material specified |
All weights, minimums and lead times here are indicative and subject to the latest quotation. One pattern holds across the lanes: Finetex Global quotes MOQ from 300 to 2,000 pieces per style in mixed sizes, and roughly a third of the programmes it takes on start below 1,000 pieces per style — which is the usual reality for a brand’s first order rather than a compromise.
Cost and MOQ Breakdown: Fabric at 45–60% and the GSM–Spandex Trade-Off
Fabric is the largest single line in a knitwear quotation, and a planning range of roughly 45–60% of garment cost is a reasonable starting assumption before labour, trim and packing are added. The exact share moves with yarn, weight, finishing and order size, so treat the range as a budgeting figure and ask for a line-item breakdown rather than a single piece price.
Weight and stretch are the two levers buyers pull most often, and they push cost in opposite directions. Raising GSM from 150 to 180 consumes more yarn per garment and increases fabric cost per piece while improving coverage and opacity. Adding elastane improves recovery and shape retention, but it also tightens the tolerance window for shrinkage, dyeing and heat setting, which raises the cost of getting the first bulk lot right. The cheapest specification on a spreadsheet is rarely the cheapest after a rejection.
Minimum order quantities follow the same logic. Stock fabric programmes can start from about 300 pieces per style, while a fully custom knit or dye lot typically begins at 1,000 pieces per colour, and both figures are indicative and subject to the latest quotation. Quotations are normally returned within one working day with fabric, labour, trim and packing shown separately, held valid for 90 days, with sample charges credited against the bulk order.
Pre-Production Testing and Quality-Control Gates Before Bulk Cutting
The most expensive defects are the ones discovered after the garments are sewn, so the effective sequence is test the fabric, approve the sample, then cut. Bulk fabric inspection covers shade continuity, shrinkage, weight per square metre and colour fastness, and it happens before the cutting table is loaded rather than after the goods are packed.
A workable gate structure has four checkpoints. First, an approved physical sample and a version-controlled specification sheet are held by both parties, so “approved” means one documented garment rather than an email thread. Second, bulk fabric is tested and signed off before cutting. Third, in-line quality checks run at roughly 30% and 70% of the run, which catches a drifting seam or waistband while the balance of the order can still be corrected. Fourth, a final random inspection at AQL 2.5 with a photo report is completed before packing and shipment.
Compliance runs alongside quality. OEKO-TEX Standard 100 is renewed annually and its scope should be matched to the materials specified, and the Standard 100 framework explains what that entry covers. Fibre claims for bamboo, Lenzing modal, TENCEL™ and recycled polyester need chain-of-custody documents, and the Global Standard publishes the organic textile criteria that such claims are measured against. Buyer-specific testing through SGS, Intertek and Bureau Veritas is common on retail onboarding programmes, and factory social audits under BSCI or Sedex are a separate file that buyers should request rather than assume.
Label and care marking is a small, high-frequency failure point. US fibre labelling requirements are set out by the FTC in its guidance on the Textile and Wool Acts and in 16 CFR Part 303, while care symbols are standardised through GINETEX. Confirm the wording and placement inside the order file at specification lock, not at the packing station.
How to Start: Sampling, Specification Lock, Then Bulk Production
The sequence that produces the fewest surprises is short: review the tech pack, build a fit sample, lock the specification, then cut. A tech pack, reference sample or competitor garment is enough to begin, and a quotation is normally returned within one working day with a cost breakdown before any sample is booked.
Development timing is the part buyers most often mis-plan. A fit or development sample typically takes 5–7 working days, and a graded size set takes 10–12 working days, with samples built from bulk fabric where the programme requires it. Those windows are working durations rather than buffers, and they are indicative and subject to the latest quotation. Version-controlled specifications and one named merchandiser per order keep the sample and the bulk order connected, and out-of-tolerance batches are corrected before shipping rather than negotiated after arrival.
Once the specification is locked, the approved sample becomes the reference for both sides, and bulk fabric is tested against it before cutting. Print, embroidery, washing, trim and retail packaging are planned under the same schedule, with export documentation, Amazon FBA preparation and weekly written production updates handled alongside. A fuller description of these capabilities sits on the Finetex Global capabilities page, and fabric development options are covered under custom fabric.
FAQ
How can a buyer verify a Chinese textile factory without travelling?
A live video walkthrough is the fastest substitute for a visit: ask to see the cutting table, the sewing lines running your garment type, the in-line inspection station and the packing area in one continuous call rather than edited footage. Then request current certificate copies with scope and validity dates, a sample made to your own specification rather than the factory’s stock style, and the names of two reference programmes with comparable volumes. A supplier that answers all four requests quickly is easier to audit later.
Can a first order mix several sizes and colours at a low volume?
Yes, within limits, and mixed sizes are usually the easy part because they come off the same cut and the same dye lot. Colour is the constraint: each additional colour on a custom knit or dye lot is normally treated as its own minimum, so adding colours multiplies the volume commitment rather than dividing it. A practical first order keeps one or two colours in stock fabric across a full size run, then adds colours once sell-through data justifies the second dye lot.
How should a shade mismatch between sample and bulk be handled?
Start from the approved physical sample, because that is the reference both parties signed off, and compare it against the bulk fabric under the same lighting rather than in different rooms. If the deviation exceeds the tolerance in the specification, the correct remedy is to reject the fabric lot before cutting, when the cost is limited to the mill, rather than to inspect finished garments afterwards. Shade continuity checks are therefore most valuable as an incoming-material gate.
Does OEKO-TEX Standard 100 certification transfer to my finished garment?
Not automatically. A Standard 100 certificate is issued for a defined product scope and material, so the buyer’s job is to confirm that the certificate covers the specific fabric or component used and that the validity dates are current, since certification is renewed annually. Where a retailer requires finished-garment testing, that is normally addressed through buyer-specific laboratory testing alongside the material certificate. Certificate numbers and scope should be filed with the order before any claim is published.
Send a tech pack, a reference garment or a target specification. Finetex Global will review the fabric route, minimum per colour and sampling plan, then return a costed quotation with each line shown separately, usually within one working day: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day