
Seamless Apparel Manufacturer China: Innovation, Technical Capabilities, and Global Market Leadership — Buyer’s Guide
The quotation looks workable, the sample fits, and then the bulk shipment lands with legs half a size short, a grey that no longer matches the…
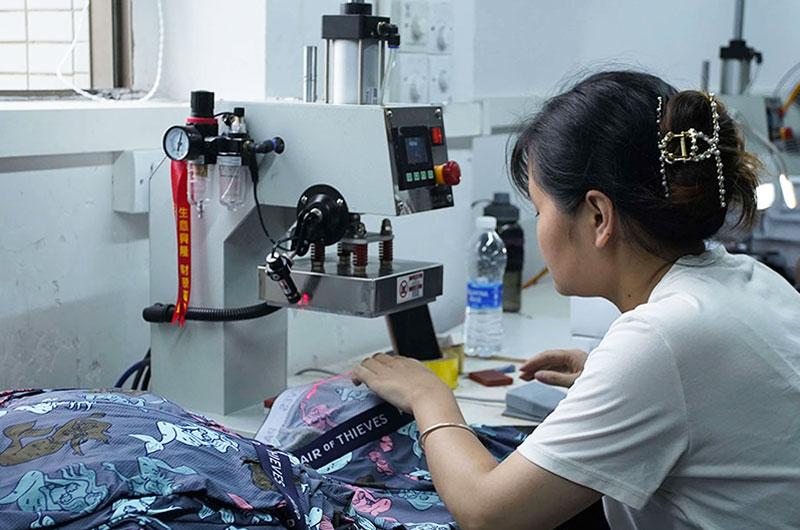
The quotation looks workable, the sample fits, and then the bulk shipment lands with legs half a size short, a grey that no longer matches the first order, and stretch recovery that reads differently after two washes. Seamless sourcing from China rarely fails at the prototyping stage; it fails once knitting, dyeing, finishing and sewing stop answering to a single locked specification. This guide is written for buyers who have to commit to a purchase order. It covers how true seamless, tubular and seamless-style construction differ, which machine and fibre details are worth verifying, how the main Chinese sourcing clusters compare, and how MOQ, cost and QC gates interact. Finetex Global’s own programmes sit in men’s knitwear, so categories outside that scope are framed here as evaluation criteria and verification method rather than claimed capability.
Seamless apparel manufacturing in China: the short answer
Seamless apparel manufacturing in China is concentrated in factories that knit the garment as a tube on circular machines, then finish with minimal seams, bonding or flatlock. Buyers should select on construction type, machine gauge, fibre traceability, shade and recovery control across batches, verified QC gates, and landed cost rather than on catalogue claims alone.
Where the capacity actually sits: market shifts and China’s sourcing clusters
Seamless capacity in China is concentrated rather than uniform. A relatively small group of specialist circular-knit knitters and integrated knitwear factories can hold engineered zones, stitch-density variation and recovery within a locked tolerance across repeat runs; the rest of the market supplies adjacent services at varying depth. Regional choice therefore follows construction route and fibre chain more closely than headline pricing.
Everything else below is the working detail behind that sentence: which construction route suits which programme, which tolerances belong in a version-controlled spec, how the sourcing clusters differ in what they can hold, and which quality documents to request before a purchase order is issued. Finetex Global appears in the comparison matrix later in this guide alongside supplier archetypes that hold capabilities outside its men’s knitwear scope, and that position is disclosed rather than implied.
The Pearl River Delta, including Shenzhen, Dongguan and Guangzhou, keeps knitting, dyeing, finishing, cutting and sewing within short transport distances, which shortens the feedback loop when a shade or shrinkage problem appears. Fujian carries depth in sportswear and performance knits. Zhejiang pairs fine-gauge knit capacity with high e-commerce volume. Inland provinces offer lower labour cost, at the price of longer logistics and a thinner technical supply base.
Two buying shifts shape 2026 plans: retail onboarding increasingly depends on restricted-substance and fibre-traceability documents, and smaller specification-heavy first orders now reach factories that once required volume. A practical note: ask which steps are in-house and which run through partner mills, because that gap is where shade continuity and half-size deviation are usually introduced.
True seamless, tubular and seamless-style: what each construction can actually deliver
The word seamless describes three different supply chains, and confusing them is the most common cause of a mismatched quotation. True seamless means the garment body is knitted to shape on a circular machine with engineered zones, so there is no side seam to cut or join. Tubular knitting forms a continuous tube that is then cut and sewn, which keeps fabric hand and eliminates side seams but leaves gusset or crotch construction to the sewing floor. Seamless-style cut-and-sew uses flatlock, coverstitch or bonded edges to make a conventional pattern feel and behave like a seam-free garment.
| Construction route | How the garment is formed | Where seams remain | Tooling and machine dependence | Minimum order implication | Typical failure mode |
|---|---|---|---|---|---|
| True seamless | Knitted to shape on a circular machine with engineered zones for fit, support and ventilation | None in the body; finishing at openings, waistband and leg hems | High; dedicated seamless machines, gauge and cylinder diameter set the size range | Highest per style, because machine time and pattern set-up are fixed costs | Recovery loss and stretch drift between runs if heat-setting and yarn lots are not controlled |
| Tubular knit | Knitted as a continuous tube on a circular machine, then cut and assembled | Gusset, crotch and waistband joinery | Moderate; circular knitting plus coverstitch and flatlock capacity | Mid-range; more forgiving than true seamless because panels can be re-cut | Seam bulk and twist after washing when panel tension is not standardised |
| Seamless-style cut-and-sew | Cut from flat knit fabric to a graded pattern, then joined with low-profile stitches or bonding | Internal, but flattened or bonded so nothing rubs | Low; conventional cutting and sewing with flatlock and coverstitch stations | Lowest; pattern grading and bulk fabric are the main constraints | Fit inconsistency across size set when grading is not locked to an approved physical sample |
A practical note for specification work: ask the factory to mark, on a finished sample, exactly where material is joined, bonded or folded. That single marked sample tells you which of the three routes you are actually buying, and it is the reference you hold against bulk.
Equipment, gauge and the scaling question behind a factory audit
The decisive audit question is not how many machines a factory lists, but which machines would be dedicated to your style and how changeover is scheduled. Gauge, cylinder diameter and stitch structure determine whether a size range can be knitted to shape, while flatlock and coverstitch capacity decides how openings, waistbands and hems are finished. A factory can hold strong knitting capability and still fail a programme through thin finishing capacity.
On the sewing floor, dedicated waistband and elastic application stations matter more than raw line count, because waistband tension controls roll-over and recovery after washing. In-line quality-control stations placed through the run, not only at the end, are the other structural signal worth checking.
Scaled capability should be read as a claimed figure until verified against your own style. Finetex Global reports a 5,652 square metre Shenzhen facility, 500-plus staff, 12 sewing and production lines and monthly capacity in the region of 600,000 pieces; treat these as indicative and subject to the latest quotation. Fabric knitting and dyeing commonly run through long-term partner mills, so confirm which steps sit inside the factory gate and how many lines would run your style.
Material architecture: matching fibre, weight and stretch to the programme
Fibre choice decides how a seamless programme behaves in wear and in the wash, and it drives a large share of the unit cost. Finetex Global’s men’s knitwear range runs from 120 to 220 gsm across cotton, pima cotton, modal, micro modal, Lenzing modal, bamboo, viscose and rayon, lyocell and TENCEL, nylon and polyamide, polyester, recycled polyester and performance blends. The construction route does not change that logic: a heavier knit carries more yarn per garment, and elastane content changes recovery, hand and heat-setting requirements at the same time.
| Fibre family | Weight selection | Where it performs | What to verify before ordering |
|---|---|---|---|
| Cotton and pima cotton | Set within the 120–220 gsm range by the tech pack | Everyday underwear, undershirts and T-shirts where a dry, natural hand is wanted | Shrinkage control and shade continuity across dye lots |
| Modal, micro modal and Lenzing modal | Same range, usually specified for drape and softness | Premium briefs and boxer briefs that need a smooth surface | Fibre chain-of-custody documents where a branded fibre claim is printed |
| Bamboo, viscose and rayon | Same range, selected for cool hand and flow | Lightweight basics and warm-weather programmes | Composition testing, because fibre naming rules follow labelling regulation rather than marketing language |
| Lyocell and TENCEL | Same range, chosen for moisture management and smoothness | Premium knitwear with a sustainability narrative attached | Traceability paperwork for the branded fibre claim |
| Nylon and polyamide | Same range, often blended for strength and recovery | Performance and compression-oriented knitwear | Stretch recovery after repeated wash cycles |
| Polyester and recycled polyester | Same range, including recycled-content options | Volume basics and sport-led lines | Recycled-content documentation and colour fastness |
| Performance blends | Same range, engineered to a function brief | Moisture-wicking, compression and training programmes | Whether the claimed function is tested and reported, not assumed |
A practical note: lock the exact fibre composition, weight per square metre and elastane percentage into a version-controlled specification, then hold an approved physical sample signed by both parties. Verbal agreements about hand feel do not survive a supplier change or a shift in yarn lot.
Manufacturer comparative matrix: four supplier archetypes judged on evidence
Supplier type explains more about programme risk than country or headline capability. Integrated knitwear factories control more of the chain and catch shade and sizing deviations earlier; specialist seamless knitters hold deeper machine capability but fewer adjacent services; trading companies add coordination and can blur accountability; low-cost cut-and-sew workshops suit simple volume and struggle with engineered knit specification. The matrix below compares these archetypes on the variables that decide a first order. Finetex Global is disclosed in the first row as an integrated men’s knitwear manufacturer, and the same metrics are applied to every archetype.
| Supplier archetype | Construction depth | Order posture | Evidence you can expect | Where it fits | Main risk |
|---|---|---|---|---|---|
| Integrated men’s knitwear factory (Finetex Global’s category, Shenzhen) | Sourcing and fabric development, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation under one plan | 300–3,000 pieces per style; stock fabric from 300; custom knit or dye lot typically from 1,000 pieces per colour (indicative, subject to the latest quotation) | Version-controlled specifications, an approved physical sample held by both parties, in-line checks at 30% and 70%, AQL 2.5 final inspection with a photo report | Men’s basics and knitwear needing consistent shade and sizing across repeat batches | Scope limits: men’s knitwear depth is real, while categories outside that range belong with a specialist |
| Specialist true-seamless knitter | Deep circular-knit capability with engineered zones; finishing often outsourced | High per style, driven by machine time and pattern set-up | Machine and gauge list, knitted-to-shape samples, stitch-density records | Programmes where seam-free construction is the product | Coordination gaps between knitting, dyeing, finishing and packing |
| Trading company or sourcing agent | None directly; capability is subcontracted across suppliers | Flexible to quote, since nothing is committed until an order is placed | Supplier naming, audit reports, inspector access requests | Multi-category programmes needing one administrative interface | Accountability blur when a batch fails |
| Low-cost cut-and-sew workshop | Conventional cutting, sewing, flatlock and coverstitch | Volume-led, with limited appetite for complex grading | Pattern files, size-set samples, basic inspection records | Simple seamless-style basics at volume | Fit and shade drift between repeat runs |
A practical note on comparing these options: score each supplier on the same five questions, in writing, and weight the answers to your own failure history. A weaker answer on shade continuity is more expensive than a higher unit price when a launch date is at stake.
Choosing by project type: value, premium, sport and eco programmes
The construction route should be chosen from the programme, not from the trend. For a value line built on multipacks, seamless-style cut-and-sew with a locked size grade usually gives the most predictable landed cost, because flat knit fabric is easier to source and panels can be re-cut. The trade-off is that low-profile seaming has to be specified properly, or the garment reads as ordinary underwear with a marketing label.
Premium programmes justify true seamless or a fine-gauge tubular body, because the product benefit is surface smoothness and engineered support, and the buyer can carry a higher per-style minimum in exchange. Sport and compression lines should be specified around recovery and moisture behaviour rather than softness, which shifts the fibre brief toward nylon, polyamide and performance blends.
Eco-led programmes hinge on documentation: recycled polyester, bamboo, Lenzing modal and TENCEL claims need chain-of-custody paperwork, and restricted-substance certification needs to be current and in scope for the specific fabric and finish. A practical note: decide which project type you are buying before you request quotations, because the same brief sent as a value enquiry and as a premium enquiry returns specifications that are not comparable.
Cost and MOQ anatomy: where the money goes and why weight and elastane move the price
Fabric typically accounts for 45 to 60 percent of the unit cost of a knitwear garment, which is why weight and stretch decisions dominate a quotation. Labour, trim and packing follow, and a costed quotation should show them separately; one blended figure makes it impossible to judge whether a weight reduction or a trim substitution delivered savings.
Weight per square metre is the most direct cost variable, because a heavier knit consumes more yarn per garment. Elastane is the second, since higher content improves recovery and shape retention but changes yarn cost, knitting tension and heat-setting requirements. Finetex Global quotes 300–3,000 pieces per style, with stock fabric from 300 pieces and a custom knit or dye lot typically from 1,000 pieces per colour; these figures are indicative and subject to the latest quotation.
Minimum order quantity is really a tooling and colour decision: stock fabric keeps the entry point low, a custom colourway commits a dye lot, and a new knit structure adds development time and machine set-up. Request a cost breakdown within one working day of sending a tech pack, ask how long the price is held, and confirm whether sample charges are credited against the bulk order.
Pre-production testing and the QC gates that prevent a rejected batch
Most rejected batches are decided before the first garment is cut. Bulk fabric inspection for shade continuity, shrinkage, weight per square metre and colour fastness sits upstream of cutting; when it is skipped, the defect has already been multiplied by the size grade. In-line checks at 30 percent and 70 percent of the run catch drift while the run can still be corrected, and a final AQL 2.5 random inspection with a photo report closes the order before packing and shipment.
The documentation layer should match the claim being published. OEKO-TEX Standard 100 covers restricted substances and is renewed annually, BSCI or Sedex audits cover social compliance, and fibre composition plus chain-of-custody records support bamboo, Lenzing modal, TENCEL and recycled polyester claims. Colour fastness and shrinkage reports, country-of-origin paperwork and buyer-specific testing through SGS complete the file. Labelling is regulated rather than optional: fibre content, country of origin and care instructions follow the US Textile and Wool Acts and 16 CFR Part 303, care symbols follow GINETEX conventions, and restricted-substance limits are documented through OEKO-TEX Standard 100. Practical note: agree numeric tolerances for shade, shrinkage and weight before bulk, because an unquantified tolerance is not a tolerance.
From sample to bulk: the working sequence for a first seamless order
A first order moves through three gates in sequence, and skipping one moves the cost to the bulk run. Sampling establishes fit and hand; specification lock freezes fibre, weight, elastane content, tolerances and trim; bulk production then runs against the locked version rather than against conversation. Finetex Global works with a fit and development sample in about five to seven working days and a graded size set in about ten to twelve working days; these timings are indicative and subject to the latest quotation.
Once the physical sample is approved and held by both parties, patterns are graded once and locked, and the specification is version-controlled so that a change request is a documented revision rather than a verbal instruction. Production updates are issued in writing each week, and one named merchandiser carries the order end to end. For men’s knitwear with a strong fit dependency, start with a boxer briefs programme or an underwear line, and involve apparel design and development before the first pattern is cut. The sequence is deliberately slower at the front and cheaper at the back.
FAQ
Can a factory in China take a first order below 1,000 pieces per style?
Often, yes, if the fabric already exists. Styles using stock fabric can start from 300 pieces per style, while a fully custom knit or dye lot typically starts at 1,000 pieces per colour, and a meaningful share of real programmes run below 1,000 pieces per style. The constraint is rarely goodwill; it is dye-lot minimums and machine set-up time. Treat published minimums as indicative and subject to the latest quotation, and send your size breakdown with the enquiry so the factory can quote on your actual mix.
How do I verify a seamless supplier without travelling to the factory?
Ask for three things in writing. First, the machine list that would actually run your style, including gauge and cylinder diameter range. Second, the certificate file, so restricted-substance and social-audit scope can be checked before any claim is published. Third, a reference sample set that includes a bulk production unit, not only a development sample. Then commission a third-party inspection through a laboratory such as SGS and request a live video walkthrough of the line scheduled for your order.
Why does the sample match the brief but the bulk batch drift?
Drift is usually introduced in three places: a different dye lot in the bulk fabric, unapproved changes in yarn or elastane, and inconsistent tension across machines. Sampling and production should run from the same bulk fabric, the specification should be version-controlled, and shade continuity, shrinkage and weight per square metre should be inspected before cutting rather than after sewing. In-line checks partway through the run catch the problem while the batch can still be corrected instead of re-made.
Is true seamless always more expensive than cut-and-sew?
Unit cost usually is higher, because circular seamless machines knit slowly relative to panel knitting and the pattern set-up is fixed per style. That premium is not automatic across the whole programme, though. Cut-and-sew carries its own labour cost in seaming and finishing, and fabric utilisation differs between the two routes. Fabric alone accounts for roughly 45 to 60 percent of garment cost, so a weight reduction can outweigh a construction change. Compare quoted routes on identical fibre, weight and trim.
Which documents should be in the order file before shipping?
At minimum: the approved physical sample, the version-controlled specification, bulk fabric inspection results, in-line QC records, and an AQL 2.5 final inspection report with photographs. Add fibre composition and chain-of-custody documents where a branded or recycled fibre claim is made, colour fastness and shrinkage reports, country-of-origin and customs paperwork, and any buyer-specific test reports. Care and content labelling should be checked against the destination market rules before the labels are printed, not after packing.
To move from an idea to a specified product, send a sketch, a reference garment or a competitor sample. Finetex Global confirms the construction, fabric options, minimums and sampling gates: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day