
How to personalize a custom boxer briefs waistband: A Manufacturer’s Walkthrough
Your launch date is fixed, the fit sample is approved, and then the banded elastic arrives in a shade that does not match the swatch you…
Your launch date is fixed, the fit sample is approved, and then the banded elastic arrives in a shade that does not match the swatch you signed off. That is the moment personalisation stops being a design decision and becomes a production control problem. A waistband carries more than a logo: it sets the top fit, the stretch recovery after repeated washing, and the labelling a retailer will check on the shelf. This walkthrough follows the sequence used on a men’s knitwear production floor, from elastic choice and branding method through cutting, attachment, testing and specification lock. All figures here are indicative and subject to the latest quotation.
Short answer: how to personalize a custom boxer briefs waistband
Personalize a custom boxer briefs waistband by choosing the band construction first, then the branding method: woven jacquard, printed or embossed elastic, a sewn-on woven label, or a printed inner-band logo. Confirm fibre content, band width, stretch and recovery targets, and care-labelling rules before you approve the sample.
Boxer briefs manufacturing: where the waistband enters the production plan
Waistband programmes are won or lost at scheduling, because the band has to be ordered, cut and attached on the same plan as the body panels, or shade and tension drift apart. The body is cut from knit fabric in the 120–320 gsm range, while the band arrives as a separate elastic or fabric-covered component with its own dye lot and its own stretch behaviour. Through the boxer briefs factory programme, dedicated waistband and elastic application stations sit alongside flatlock and cover-stitch capacity, so the band is treated as a controlled part rather than a trim bought late.
Everything after that answer is execution detail. Band construction comes first because it constrains what can be woven, printed or embossed on the surface, and because it sets the tension the pattern was graded to. A narrow plush-back band behaves differently from a wider smooth band under the same pouch and rise, so substituting one for the other normally forces a fit re-approval rather than a colour tweak. Write the band type, width, fibre content and branding method into the version-controlled specification, and keep one approved physical band in the order file before the first cut.
Volume is quoted per style: from 300 pieces on stock fabric up to 3,000 pieces mixed across sizes, with a fully custom knit or dye lot typically starting at 1,000 pieces per colour. Those ranges are indicative and subject to the latest quotation. Place the elastic purchase order alongside the fabric order so both lots are recorded once, against one approved standard.
Custom boxer briefs: the specification variables a brand actually controls
Personalisation is a stack of decisions, and the waistband is only the most visible layer. A buyer controls the inseam (3–9 inch), the pouch shape (contour or standard), the rise, the fabric family — cotton, pima, modal, micro modal, Lenzing modal, bamboo, viscose, lyocell or TENCEL™, nylon and polyamide, polyester, recycled polyester and performance blends — the fabric weight, and the band. Move the fabric weight or the elastane content of the band and the fit approved in the size set may no longer hold at the top of the garment, which is why grading is locked once and re-opened only when a specification genuinely moves.
| Method | How the branding is produced | Setup and tooling | Suited to | Lock in the tech pack |
|---|---|---|---|---|
| Jacquard woven elastic | Logo woven into the band during elastic manufacture | Pattern tooling and colour repeat at the elastic mill | Multipack and retail programmes with repeat orders | Colour count, repeat length, band width, fibre content |
| Silicone or rubber print | Printed or transferred onto the band surface | Print screen or transfer plate per design | Sport and gripper programmes | Placement, coverage area, cure and wash testing |
| Sublimated or heat-transfer elastic | Full-colour graphic applied by transfer | Artwork file, per-order preparation | Seasonal graphics and small colour runs | Artwork version, colour tolerance, wash fastness target |
| Embossed or debossed logo | Relief pressed into the band with a heated die | Engraved die matched to band surface | Premium programmes with restrained branding | Die depth, band surface type, tread pressure |
| Sewn-on woven label | Label stitched at centre back | Label artwork and cut, no elastic tooling | Low-volume runs and rebranding existing stock | Label position, stitch type, label size |
| Printed inner band | Ink printed on the inside face of the band | Print plate plus skin-contact material check | Comfort-led programmes without outer branding | Ink type, coverage, certification of the printed band |
Ask for every branding method to be proven on a bulk-fabric band rather than a plain sample band, because print adhesion and emboss depth both change with the surface finish of the elastic.
Inside the factory: what a waistband programme runs through
Control matters most at the handover points rather than in the headline number, and the waistband is exactly such a handover. At Finetex Global, a men’s knitwear OEM/ODM manufacturer in Shenzhen whose legal entity is Finetex Textile Co., Ltd., fabric sourcing and development, sampling, cutting, sewing, printing and packing answer to one production plan, which means an elastic lot that arrives off-shade is caught at incoming inspection instead of after the bands are sewn on. Factory operations in Shenzhen cover 5,652 m², and the company has manufactured men’s knitwear for export since 2004.
The men’s underwear manufacturing line carries waistband and elastic stations, flatlock and cover-stitch capacity, and in-line inspection points, so a band issue can be isolated by lot. One named merchandiser holds the file, and written production updates go out weekly. Figures quoted for volume and timing are indicative and confirmed against the latest quotation.
Automatic fabric cutting: the step that decides shade continuity
Automatic cutting will not rescue a bad band lot, but it makes a good one repeatable. Panels are spread and cut to a marked plan, which keeps the panel shapes consistent across the size set, while the band is cut from elastic rolls where a few millimetres of width variation or an over-stretched roll visibly changes the finished top edge. Because knit fabric relaxes and shrinks, the bulk fabric is inspected before cutting for shade continuity, shrinkage, weight per square metre and colour fastness against the approved standard.
Three points matter commercially. Narrower bands consume less elastic per piece but leave less surface for branding; wider bands read more strongly on the shelf and consume more material; and a band supplied in a different dye lot from the approved sample is a rejection risk that no cutting plan can absorb. Approve the cutting plan and the band roll width together, and hold a retained band from the bulk lot in the order file.
Underwear elastic attachment: stitch, tension and recovery
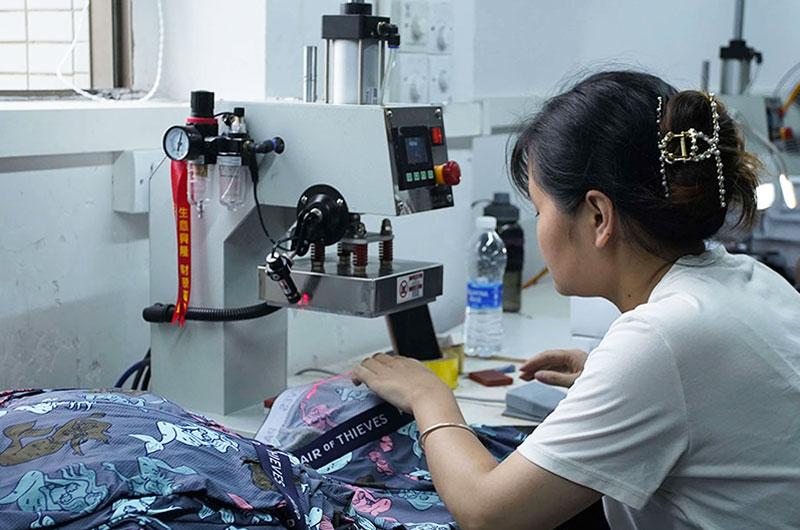
The attachment step is where a personalisation decision becomes a comfort decision. Bands are joined to the body with flatlock or cover-stitch construction on knit underwear, with the stitch type, thread and tension set so band and body stretch together instead of fighting each other. Centre-back joins and bartacks are placed where the specification puts them, which is what keeps a band from twisting or rolling after laundering.
Trade-offs run in opposite directions. A firmer band holds a printed or embossed logo sharply but can feel stiff over the hip bone, while a plush-backed band feels softer against skin but may take a lighter relief. Attachment quality is checked in-line at 30% and 70% of the run, then by AQL 2.5 final random inspection with a photo report before packing. Because care symbols after repeated washing are a labelling obligation, confirm care instructions and the relevant GINETEX symbol set before the care label is printed.
FAQ
Can wearing tight boxers cause testicular pain?
A waistband that is too tight and a shallow pouch can cause chafing, pressure and a feeling of heaviness, but garment fit is not the same thing as a diagnosed medical cause. Clinical assessment of testicular pain looks first at torsion, infection, injury and other conditions, and sudden or persistent pain needs medical attention rather than a change of underwear. From a manufacturing side the controls are band tension, pouch depth and rise, plus a wash test that confirms the band does not tighten after laundering.
What is the slit in boxer briefs for?
The vertical opening at the front is a functional fly, and on many modern pairs it is closed with a stitched or bonded overlap rather than a button or buttonhole. It exists for convenience, but it also changes construction: a fly adds a panel, a bartack and a fold, and it alters how the pouch sits. Comfort-led ranges sometimes remove it, because a contoured or seamless pouch draws a cleaner line. Fly or no fly is a pattern decision, so settle it in the tech pack.
How long does it take to make custom boxers?
For a first programme, plan on roughly one week for a development sample and about two weeks for a graded size set, with bulk production following specification approval. At Finetex Global the indicative windows are 5–7 working days for a fit sample and 10–12 working days for a size set, built from the bulk fabric where it is available. Bulk timing then depends on fabric, elastic and print lead times, so every figure is indicative and subject to the latest quotation.
How can I make my own boxer shorts?
For personal use, boxer shorts need a pattern, a knit fabric, an elastic band and a basic sewing machine, and the result depends mostly on the pattern you start from. Turning that into a sellable programme is a different exercise: you need a graded pattern, a defined band and fabric, fibre and care labelling that meets the Textile Fiber Products Identification Act and 16 CFR Part 303, and testing before retail. Most brands begin from a reference sample instead of a home pattern.
Sourcing by project type: value, premium, sport and eco programmes
The right waistband is the one that fits the price architecture of the programme, not the most decorated option available. A value multipack usually runs a plain or single-colour jacquard band with one print colour, standard fabric weights and tight shade control across the run. A premium range justifies an embossed or debossed logo on a plush band with modal, micro modal or pima fabric, where the cost sits in the fabric and the die work rather than in decoration. A sport programme needs a silicone gripper band, nylon, polyamide or performance blends, and a verified claim trail. An eco programme needs certified fibre chain-of-custody documents, recycled polyester or bamboo and lyocell options, and fibre labelling that matches the certificate.
Finetex Global is a men’s knitwear manufacturer writing from that position, and the criteria above are the ones its team applies when costing a programme. Bring the price target to the band discussion, and settle design ownership and MOQ implications in writing where a brand’s own artwork is involved — our note on ODM men’s clothing design rights and MOQ covers how that is handled.
Cost and MOQ: where the waistband money goes
Fabric typically accounts for 45–60% of unit cost in a men’s underwear programme, with labour, trim (including the band) and packing making up most of the remainder, so a waistband specification is a cost conversation before it is a design conversation. A costed quotation issued within one working day shows those elements separately, which lets a buyer see immediately what a heavier fabric weight or a higher elastane content does to the unit price. Indicative figures only, subject to the latest quotation.
The trade-offs are consistent. Higher grams per square metre and higher elastane content raise both comfort and cost, a wider band consumes more elastic per piece, and a multi-colour jacquard adds tooling plus a minimum per colour. MOQ moves with the fabric decision: stock fabric can start from 300 pieces, while a fully custom knit or dye lot typically starts at 1,000 pieces per colour, and programmes are usually quoted up to 3,000 pieces per style across mixed sizes. Those quantities are indicative and subject to the latest quotation; quotations are held for 90 days, and sample charges are credited against the bulk order.
Pre-production testing and the QC gates that stop a rejected batch
Testing is scheduled rather than improvised, and the band is verified before the body is cut, not after the garments are finished. Bulk fabric inspection covers shade continuity, shrinkage, weight per square metre and colour fastness against the approved standard; on the floor, in-line checks run at 30% and 70% of the production run, and AQL 2.5 final random inspection with a photo report happens before packing and shipment. A physical approved sample is held by both parties and the specification is version-controlled, so a change of band or branding method cannot travel unnoticed.
On compliance, OEKO-TEX Standard 100 coverage is renewed annually, fibre composition and chain-of-custody documents are available for bamboo, Lenzing modal, TENCEL™ and recycled polyester, and buyer-specific testing can be arranged with SGS. The band print and care label also have to match the rules for fibre content, country of origin and care instructions set out in the FTC’s guidance on textile labeling and in 16 CFR Part 303, and material claims such as OEKO-TEX should be traceable to the certifying standard before they are published. Ask for the test plan as a document at quotation stage.
How to start: sampling, specification lock, bulk production
Start from a reference rather than a brief written from scratch, because a sketch, a competitor sample or a tech pack is enough to open a development file. A fit or development sample is quoted at 5–7 working days and a graded size set at 10–12 working days, with samples built from the bulk fabric where it is relevant. All indicative and subject to the latest quotation.
Specification lock is the second gate: band width, branding method, fibre content, shade standard, care label text and packaging are frozen against the approved physical sample. Only then does bulk production run, under one named merchandiser with weekly written updates and the QC gates described above. Quality control documents, sample approvals and test reports travel with the order, and development support sits with the apparel design team from first artwork to final band.
Send a tech pack, a reference garment or a target specification. Finetex Global will review the fabric route, minimum per colour and sampling plan, then return a costed quotation with each line shown separately, usually within one working day: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Men’s underwear manufacturer
- Boxer briefs factory
- Apparel design and product development
- Quality control and inspection
- ODM men’s clothing: design rights and MOQ
It sits inside the wider underwear fit and fabric specifications, where the rest of the sequence is set out.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day