
What Is Cotton Polyester Fabric and Why Is It Popular: A Production-Side Explanation
A 60/40 cotton-polyester tee is approved, the bulk lands three weeks before a retail window, and the second dye lot reads half a shade warmer than…
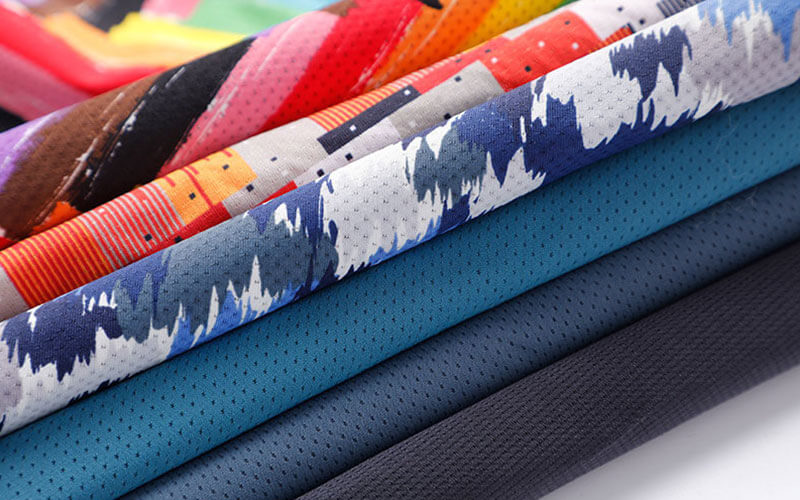
A 60/40 cotton-polyester tee is approved, the bulk lands three weeks before a retail window, and the second dye lot reads half a shade warmer than the first. Cutting has already started, so the real question is not which blend to use but which fibre ratio, yarn type and finishing route the specification locked in before the order was placed. That is the practical version of what is cotton polyester fabric and why is it popular: a blend engineered for lower unit cost than pure cotton, faster drying and better dimensional stability, at the price of extra discipline in dyeing, hand feel and labelling. This guide covers how the blend behaves on the production floor, where the money sits, and how to specify it so shipment two behaves like shipment one.
The short answer: what the blend is on a production line
Cotton polyester fabric is a blend of cotton and polyester staple fibres spun into one yarn, typically at 65/35, 60/40 or 50/50, then knitted into jersey, rib or fleece. Buyers specify it because it dries faster, shrinks less and costs less per metre than 100% cotton while keeping a softer hand than pure polyester.
A one-stop plan: what a single production schedule actually controls
Cotton-polyester programmes rarely fail inside a sewing line; they fail in the gaps between suppliers. When fabric, trims and finishing are bought separately, a shade standard agreed with one mill can disagree with a rib ordered from another, and nobody owns the difference until the pieces are cut. Running fabric development, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation under one production plan is the mechanism that removes those gaps.
The trade-off is registered at the dyehouse and in the care label rather than on the hanger. Because polyester is thermoplastic and cotton is not, the two fibres exhaust dye at different rates, so an approved shade has to be judged on the bulk fabric under the lighting the buyer actually sells under, not on a lab dip built from single-fibre yarn. Composition also has to be declared honestly: percentage by weight, generic fibre names, and order of predominance, as set out in the FTC labelling guidance and 16 CFR Part 303. In practice, lock ratio, yarn type and weight per square metre in the same conversation, because moving one shifts hand feel, shrinkage and cost together.
Finetex Global, the trading name of Finetex Textile Co., Ltd., has produced men’s knitwear for export from Shenzhen since 2004, with the published scale of a 5,652 m² facility, 12 sewing lines and monthly capacity in the region of 600,000 pieces; those figures are indicative and subject to the latest quotation. Knitting and dyeing are handled through long-term partner mills, with shade, weight and shrinkage standards agreed against the bulk order and checked before cutting begins. For buyers developing a blend from scratch, that route starts at custom fabric development.
Where quality is decided: fibre lot, stitch and the approved standard
Complaints on blended knits cluster in three places: a fibre-lot change between shipments, a shade step between rolls in the same lot, or a drift in weight and stitch density. Each is preventable, but only if the specification is written down and a physical reference exists that both sides hold. A verbal target of “about 170 gsm, similar to the last order” cannot be audited by anyone.
On that basis, a workable quality system uses version-controlled specifications, an approved sample retained by both buyer and factory, and bulk fabric inspection before cutting that covers shade continuity, shrinkage, weight per square metre and colour fastness. In-line checks run at 30% and 70% of the run so a fault is caught while the balance of the order is still open, and the final random inspection is carried out at AQL 2.5 with a photo report issued before packing and shipment. The practical ask for a buyer is simple: confirm which gate stops production, not just that inspection exists.
From a reference garment to a producible cotton polyester specification
Creative direction only becomes useful once it survives contact with a knitting machine. A competitor sample, a wash reference or a colour from a mood board can all be developed, but each one has to be translated into a fibre ratio, a yarn count, a stitch structure and a finishing route before a price means anything. Design intent that is never written as a numeric spec is where sampling costs multiply.
The translation work is tech pack review, pattern making, grading, fit correction and fabric matching, followed by print, embroidery or wash development where the design needs it; Finetex Global has run in-house fabric structure and functional knit development since 2014. Sampling on that basis typically takes 5-7 working days for a fit or development sample and 10-12 working days for a graded size set, built from the bulk fabric where the construction allows, with sample charges credited against the bulk order. Timelines such as these are indicative and subject to the latest quotation. Practically, send a reference garment together with the target ratio, weight and care claim, because the fabric decision constrains everything that follows it.
Flexibility that shows up in MOQ, colourways and size curves
Flexibility is a number, not a service adjective. The honest answer to “can this run lower?” depends on whether the fabric already exists: a style using stock fabric can start from 300 pieces, while a fully custom knit or an exclusive dye lot usually starts at 1,000 pieces per colour. Across the men’s knitwear range the working minimum is 300-3,000 pieces per style in mixed sizes, and roughly a third of programmes begin below 1,000 pieces per style. Those ranges are indicative and subject to the latest quotation.
In men’s knitwear that flexibility is routine across men’s underwear programmes, undershirts, T-shirts, tanks, polos, sweats and sportswear, and it extends into specific constructions such as the boxer briefs factory lines where narrow size curves are common. Two areas sit outside that scope: women’s lingerie and denim are not men’s knitwear programmes, so they belong with a specialist. The practical lever for a small first order is the colourway list, since consolidating three colours into two keeps a low-volume run inside a single dye lot.
Cost and MOQ: where the money in a cotton polyester programme sits
On a men’s knit top, fabric typically accounts for roughly 45-60% of the unit cost, so ratio, weight and colourway list decide most of the price before labour is discussed. A quotation is far easier to negotiate when it is itemised, which is why cost breakdowns show fabric, labour, trim and packing as separate lines, and why a quotation can be held for 90 days rather than re-priced after a yarn movement.
The trade-offs are mostly arithmetic. Raising a jersey from 160 to 180 gsm increases fabric consumption per piece roughly in proportion, and the heavier body then needs a coordinated rib and neck tape or it will distort. Adding elastane improves recovery on fitted garments, but it introduces another component to dye and test, so it must be justified by fit. A custom dye lot spreads development cost across a minimum run, which is why 1,000 pieces per colour is common. Cost is usually taken out by matching weight to season and trimming the colourway list, not by downgrading yarn quality. All figures here are indicative and subject to the latest quotation.
FAQ
Why is everyone getting rid of polyester?
Most of that movement is about market positioning, not fabric failure. Brands remove polyester to support recycled or single-fibre claims, because a 100% cotton or 100% recycled-cotton label is simpler to market and to trace than a blend, and because some retailers set fibre preferences for their own sustainability targets. The practical cost is performance: blends hold shape, dry faster and resist shrinking, so a brand that drops polyester often has to add elastane or a heavier construction to recover the fit. The decision is commercial and garment-specific, not a verdict on the fibre.
Is 80% cotton 20% polyester good quality?
An 80/20 split is a recognised commercial build and can be well made or poorly made depending on the yarn, the weight and the fabric’s dimensional stability. With a higher cotton share you keep more moisture absorbency and a cotton hand, while the polyester portion adds strength and reduces shrinkage; the usual risk is a slightly less uniform surface if low-grade yarn is used to hit a price. Judge it on the approved sample, the declared composition, the weight per square metre and the shrinkage report rather than on the ratio alone.
What is the unhealthiest fabric to wear?
There is no single unhealthiest fibre, because the risk comes from what is applied to a fabric rather than from the fibre name. Dye residues, formaldehyde-based finishes and certain azo colourants are the substances regulators and certification schemes actually restrict, which is why harmful-substance limits matter more than a cotton versus polyester argument. For skin-adjacent knitwear, buyers commonly specify certified low-residue fabric, check odour and breathability in wear trials, and keep finishes minimal. Comfort complaints on polyester-heavy garments usually relate to heat and moisture retention, which construction and weight can address.
What’s better, 100% polyester or 100% cotton?
Neither is universally better; the garment and the use case decide. Pure cotton gives moisture absorbency and a natural hand that suits undershirts, retail basics and print-heavy tees, but it can shrink and takes longer to dry. Pure polyester gives faster drying, higher tear strength and cost efficiency, which suits performance layers and linings, though it retains odour and traps heat against the skin. A blend is often the middle route for a knit that must hold its fit through repeated washing, and composition must still be declared accurately on the label.
Choosing a build by programme type: value, premium, performance, recycled
The ratio that suits a programme is decided by the retail price band, the wash behaviour the customer expects and the documentation the retailer requires, not by a general preference for more cotton. Value multipacks optimise cost per metre, premium basics optimise hand feel consistency, performance programmes optimise recovery, and recycled programmes optimise traceability. The table below sets out planning ranges for each, and every line in it is indicative and subject to the latest quotation, since yarn prices and certification scope move with the market.
| Programme type | Typical fibre split | Weight guidance | Specification to lock first | Cost and MOQ note |
|---|---|---|---|---|
| Value basics, private label and multipacks | 65/35 or 60/40 cotton-polyester, carded or open-end yarn | 150-170 gsm jersey | Shade standard approved on bulk fabric | Lowest fabric cost per metre; stock fabric can start from 300 pcs |
| Premium retail basics | 50/50 or 60/40, combed ring-spun yarn | 160-200 gsm | Yarn type and shrinkage behaviour | Higher yarn cost for hand-feel consistency; custom dye lot typically 1,000 pcs per colour |
| Performance, sportswear and compression | Polyester-dominant blend with elastane | 180-220 gsm | Recovery and wet-to-dry dimensional stability | Elastane adds a component and extra dyeing complexity |
| Recycled and traceable programmes | 50/50 or 60/40 with certified recycled polyester | 150-190 gsm | Chain-of-custody documents before the order | Documentation and certification scope affect price and lead time |
A useful habit is to read the table backwards: start from the weight the customer will feel, then work out which ratio and yarn can carry that weight at a price the channel accepts. A 200 gsm body built on cheap yarn often reads worse in the hand than a 170 gsm body built on combed yarn, even though it costs more to produce.
Pre-production tests and QC gates that can be evidenced
Tests only have value when they sit at a gate that can stop production. Reported numbers are usually a summary of a fabric inspection or a final audit, and a buyer comparing two suppliers should ask where each measurement is taken, what the acceptance rule is, and what happens when a result falls outside it. A test that is run after cutting cannot protect the order.
The gates that hold on a blended knit programme are bulk fabric inspection before cutting, covering shade continuity, shrinkage, weight per square metre and colour fastness; in-line checks at 30% and 70% of the run; and a final random inspection at AQL 2.5 with a photo report before packing. Substance limits are typically verified through OEKO-TEX Standard 100, renewed annually, with chain-of-custody documents for recycled polyester, bamboo, Lenzing modal and TENCEL™ fibres, and buyer-specific testing routed through laboratories such as SGS, Intertek or Bureau Veritas. Care instructions follow the GINETEX symbol system. The practical step is to name these gates in the purchase order rather than rely on a general quality clause.
Starting a programme: sample, lock the spec, then bulk
A blended knit programme that starts well is mostly a question of sequencing: the fabric decision precedes the fit, and the colourway precedes the dye lot booking. Buyers who send a tech pack, a reference garment or a competitor sample receive a costed quotation within one working day, with fabric, labour, trim and packing shown separately. Quotation turnaround, sample timing and MOQ are indicative and subject to the latest quotation.
The workable sequence is: development sample at 5-7 working days, graded size set at 10-12 working days, then specification lock covering fibre ratio, weight, shade standard, care label copy and packing. Bulk production follows with one named merchandiser per order and weekly written production updates, closing with final inspection and the export documentation set. Each stage leaves a document that can be checked, which is what makes a second shipment repeatable.
Planning a first or repeat order? Send the style details, size breakdown and destination market, and Finetex Global will return a costed quotation with sampling lead times stated: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- China clothing factory myths: what’s true and what to verify
- Custom fabric development for men’s knitwear
- Men’s underwear manufacturing
- Boxer briefs factory programmes
- OEKO-TEX Standard 100 harmful-substance limits
For the surrounding decisions in the same programme, see the the apparel fabric selection guide.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day