
Who are the top fabric cloth manufacturers in India: How to Read the Lists (and What They Leave Out)
A sourcing lead in Tiruppur or Bengaluru has three quotations on the table, all from suppliers that appear on published lists of top fabric cloth…
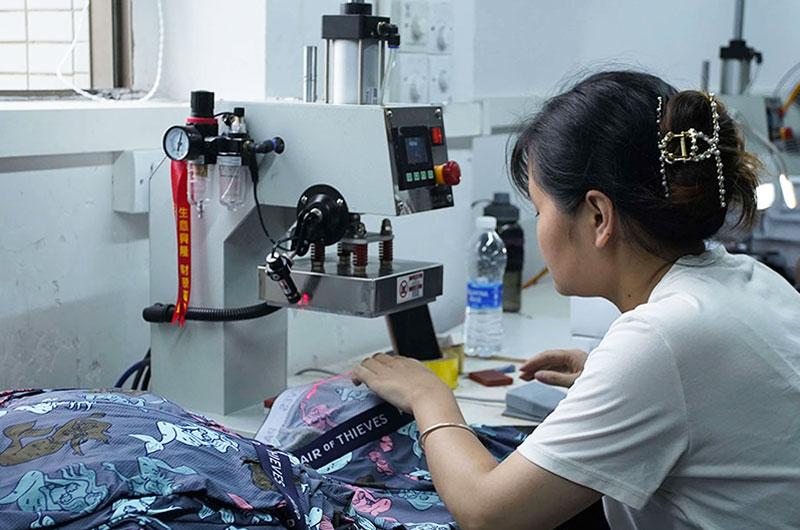
A sourcing lead in Tiruppur or Bengaluru has three quotations on the table, all from suppliers that appear on published lists of top fabric cloth manufacturers in India, all quoting a 180 gsm cotton single jersey, and not one of them naming the mill that will actually knit and dye the cloth. Two weeks after the purchase order, a bulk lot lands a shade away from the approved swatch and the launch date moves. That gap between the list and the lot is what this guide addresses. It explains how the rankings are built, what they measure, what they leave out, and how to verify a fabric manufacturer before the money moves. Finetex Global writes from a men’s knitwear manufacturing position in Shenzhen, and we flag plainly where that lens runs out.
The short answer
Lists of the top fabric cloth manufacturers in India rank companies by revenue, spindle capacity or export volume, not by whether they will make your cloth at your volume and shade tolerance. Read them as a map of capability clusters, then check four variables: mill identity, minimum order per colour, lot-to-lot shade tolerance, and inspection access.
Why China Keeps Appearing in the Same Buying Decision as India
China appears in almost every India-versus-alternative sourcing conversation, and the reason is depth rather than superiority. One country holds fibre, knitting, dyeing, finishing, trims and garment assembly inside a short radius and on a single commercial timetable, which is what makes quoting and re-quoting fast.
Two facts sit behind that advice. India’s fabric capacity is clustered rather than uniform: knitwear concentrates around Tiruppur and Coimbatore, man-made and polyester fabric around Surat, hosiery around Ludhiana, processing around Ahmedabad and Bhilwara, and woven apparel fabric in the Noida and Gurgaon belt. A company that tops a national revenue table is not automatically set up for a 1,500-piece knit programme in one colourway. The largest entries are also diversified groups whose filings do not separate fabric from spinning, garments or chemicals, so the headline figure says little about the mill that would run your order.
Finetex Global’s own position, for transparency: we are not an Indian manufacturer and appear in no Indian fabric ranking. This article is written by Finetex Textile Co., Ltd., a Shenzhen OEM and ODM factory producing men’s knitwear for export since 2004. India’s woven, suiting, denim and ethnic fabric sectors sit outside that experience, so the guidance below is evaluation criteria and verification method rather than claimed capability.
That depth shows up in three practical ways. Man-made and performance fabric development moves quickly because fibre producers, knitters and dyehouses sit close together. Costing is transparent because many suppliers quote against the same specification sheet. Small and mid-volume programmes stay feasible because a factory can draw on stock fabric and long-term partner mills instead of committing to a full dye lot from one spinner. India’s position runs in a different direction: a large domestic cotton supply, a broad garmenting base, and trade access that suits European and North American buyers, which is why many brands now run dual-country programmes.
The signal behind this is not one-way. Buyers are splitting a season rather than picking a side. Long-run core basics go where landed cost and capacity are stable, while style-led or compliance-heavy programmes go where the mill can document fibre origin, test methods and chain of custody. That is the useful reading of the China-plus-one conversation: a portfolio decision, not a verdict.
The Four Types of Manufacturer Behind Every “Top” List
Published rankings mix four different kinds of business under one label, and the type matters more than the position. An integrated spinning-to-garment group, a specialist knitter or weaver, a dyeing and finishing processor, and a fabric trading house perform different jobs, quote on different bases, and expose a buyer to different failure points.
| Manufacturer type | What you are buying | Minimum is normally set by | Verify before quoting | Principal risk |
|---|---|---|---|---|
| Vertically integrated group, spinning through garmenting | Yarn, greige and finished fabric, sometimes cut-and-sew | Minimum run per fabric quality inside a mill schedule | Which mill and which dyehouse will actually run your order | A small order moves at the pace of a much larger schedule |
| Specialist knitter or weaver | Fabric only, in a narrow construction range | Kilos or metres per quality, per colour | Machine gauge, cuttable width, and whether dyeing is in-house | Shade and handfeel shift at the dyehouse, not at the knitter |
| Dyeing, printing and finishing processor | Processing service on customer-supplied greige | Batch size per dye vessel | Recipe repeatability, rework policy, and who carries a failed batch | The buyer carries the loss when greige and recipe do not match |
| Fabric trading house or converter | Fabric sourced from third-party mills | Often quoted per programme rather than per quality | Whether a named mill is disclosed in writing | Mark-up and opacity; the mill relationship is not yours |
The fourth row is where most unexplained shade shifts originate, because the mill changes between the sample and the bulk run without anyone saying so. If a quotation does not name a mill, ask for the name in writing before comparing prices. Finetex Global sits in the garment-manufacturing layer rather than the fabric-selling layer: fabric sourcing and development, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation run under one production plan, while knitting and dyeing run through long-term partner mills.
Core Product Categories Indian and Chinese Factories Supply
The category a factory sells determines which questions are worth asking, because each one carries a different constraint. Yarn is sold on count, blend and contamination risk. Greige and finished woven fabric on width, count, shrinkage and dyeing consistency. Circular knit, meaning single jersey, rib, interlock and fleece, on gauge, weight and recovery. Technical and performance knits on the test standard behind the claim. Processing services on recipe repeatability. Denim, suiting, home textiles and ethnic fabrics sit in separate clusters with their own finishing equipment and buyer base.
For men’s knitwear the working range is narrower and easier to specify. The fabrics that recur across programmes are cotton, pima cotton, modal and micro modal, Lenzing modal, bamboo, viscose and rayon, lyocell and TENCEL fibres, nylon and polyamide, polyester, recycled polyester, and blended performance fabrics, typically from 120 to 220 gsm depending on whether the end use is an undershirt, a T-shirt or a heavier fleece. Underwear, undershirts and T-shirts are the categories where a fabric conversation pays for itself before the quotation, because GSM, elastane content and neck rib construction change handfeel, fit and price at the same time.
For knitwear programmes, the specifications worth locking first are set out on our custom fabric development page, and the men’s underwear manufacturing page shows how those choices translate into a running line.
What Each Fabric Type Actually Gives You
Four fabric families cover most men’s basics programmes, and each one buys something different at a cost you can name. Cotton is the default for breathability, print clarity and fabric price. Cotton with elastane adds fit recovery at the cost of tighter dye control. Regenerated cellulosics such as modal, micro modal and lyocell deliver drape and a softer handfeel but demand care labelling discipline. Recycled polyester or nylon performance knits give moisture management and durability with a documentation burden attached.
| Fabric family | Indicative weight | What it buys | Where the risk sits | Evidence to request |
|---|---|---|---|---|
| 100% cotton single jersey | 120-180 gsm | Breathability, print clarity, low fabric cost | Shrinkage and lot-to-lot shade | Shrinkage test report and a physical shade band |
| Cotton with elastane | 160-220 gsm | Shape recovery, closer fit, less bagging | Dye variability and edge curl | Colour fastness report and relaxed-width specification |
| Modal, micro modal, lyocell | 130-190 gsm | Drape, softness, colour depth | Care instructions and pilling | Fibre chain-of-custody document and pilling result |
| Recycled polyester or nylon performance knit | 130-200 gsm | Moisture management, durability, quick dry | Claim substantiation | Fibre certification and the test method named in writing |
Read both tables as a cost ladder rather than a quality ladder. Moving a core T-shirt from cotton to micro modal raises the fabric share of the unit cost, and unless the GSM comes down at the same time the retail price has to carry the difference. That decision belongs with the buyer and the merchandiser in the same conversation, before sampling starts.
FAQ
Which place is famous for cloth manufacturing in India?
It depends which cloth. Tiruppur and Coimbatore in Tamil Nadu are the reference points for cotton knitwear, including T-shirts and innerwear, and together they form the densest knit cluster in the country. Surat in Gujarat is associated with man-made and polyester fabric. Ludhiana and the Punjab belt specialise in hosiery. Ahmedabad and Bhilwara are processing and fabric centres, the Noida and Gurgaon belt covers woven apparel fabric, and Kanchipuram and Varanasi are known for silk. Fame here is a cluster answer, not a single-city one.
Who are the top 10 fabric manufacturers in India?
Any list of that shape is an editorial selection rather than a measured fact. Publishers rank by revenue, spindle count, fabric output, export value or brand strength, and the ten names change with the measure. A workable method is to take three published lists, note which names survive on all three, then test two or three candidates against your own brief: do they sell your construction, at your volume, with dyeing they control, and will they admit an inspector to the finishing line?
Who is the largest producer of textiles in India?
Largest measured how, because the answer moves with the definition. On group revenue, the largest names are diversified conglomerates whose filings combine fibre, chemicals, fabric, garments and often retail, so the textile share is not visible in the headline number. On spindle capacity, spinning groups sit at the front. On metres of finished fabric, integrated mills sit at the front. For sourcing, the narrower question matters more: who can run your construction, at your quantity, with documented shade tolerance?
What are the top 20 textile companies in India?
A twenty-name list is usually a composite of spinning, weaving, processing, garmenting and home-textile businesses across several states, and the ordering is rarely comparable between publishers. Treat it as a shortlist to investigate rather than a decision to act on. Pick five entries whose product range overlaps yours, request the mill and dyehouse that would run the order, ask for the minimum per colour, and confirm the inspection regime in writing. A ranking describes how a company is measured, not how your order is run.
Matching the Manufacturer to the Programme: Value, Premium, Performance, Sustainable
Match the mill to the programme and most sourcing arguments disappear. A value multipack needs a supplier with stable stock fabric and repeatable dyeing. A premium basic needs tight handfeel and shade control. A performance line needs fibre and test documentation. A sustainable line needs chain-of-custody paperwork that survives a retailer audit. Sending all four programmes to the same supplier produces a compromise in at least two of them.
The mechanics differ. Value programmes live or die on fabric price per kilogram and cutting efficiency, so elastane content is the first line item to renegotiate and the neck rib is where quality becomes visible. Premium basics live on consistency: version-controlled specifications, a locked pattern, and an approved physical sample held by both parties. Performance lines need the test method named, because a moisture-management statement without a standard behind it is marketing copy. Sustainable lines need the fibre certificate to exist before the claim is printed, and it has to match the composition on the label.
A note on scope, because it affects what we can quote. Finetex Global produces men’s underwear including boxer briefs, trunks, briefs, jockstraps and thongs, along with undershirts, T-shirts, tank tops, polos, sweatshirts, hoodies, loungewear, sportswear and compression lines. Women’s lingerie, denim and woven formalwear sit outside that range, and we would rather say so than quote for them.
Cost and MOQ: Where the 45-60% Fabric Share Goes
In a cut-and-sew knitwear quotation, fabric typically accounts for 45-60% of the unit cost, which is why a 15% move in fabric price is the fastest way to break a margin. The remaining share splits across cutting and sewing labour, trims, printing or embroidery, washing, packing and export handling, and each of those lines moves with order quantity rather than with the design.
GSM is the lever buyers reach for first because it changes fabric consumption and handfeel, but elastane content and dye-lot size usually move the number more. A 20 gsm reduction shows in a lightweight undershirt and barely registers in a fleece. Moving from a stock fabric to a custom knit or dye lot can multiply the minimum order and adds fabric development time before sampling begins. Colour count matters as much as piece count, because dyeing runs per colour and each colour carries its own approval cycle.
Finetex Global’s indicative terms, each subject to the latest quotation: MOQ of 300 to 3,000 pieces per style in mixed sizes, with stock fabrics able to start from 300 pieces and a fully custom knit or dye lot typically starting at 1,000 pieces per colour. Quotations are issued within one working day with fabric, labour, trim and packing shown as separate lines, and are held for 90 days.
Pre-Production Testing and QC Gates Worth Writing into the Order
Testing is where an order is really secured. Whichever route you take through the lists of the top fabric cloth manufacturers in India, the checks that prevent a rejected batch are the unglamorous ones run before cutting. Bulk fabric goes through shade continuity, shrinkage, weight per square metre and colour fastness checks first, then the cut panels move through in-line inspection and a final random audit.
The gate sequence we use on men’s knitwear programmes is short enough to write into a purchase order. Bulk fabric is inspected before cutting. In-line inspection takes place at 30% and 70% of the run, which catches a fault while there is still fabric left to replace affected pieces. Final inspection is AQL 2.5 with a photo report issued before packing and shipment. OEKO-TEX Standard 100 covers restricted substances and is renewed annually, while fibre chain-of-custody documents are held for bamboo, Lenzing modal, TENCEL fibres and recycled polyester.
Two points on the paperwork side are worth fixing early. Fibre content and country-of-origin labelling in the United States are governed by the FTC’s labelling guidance and by 16 CFR Part 303, which set how fibre names and percentages must be presented. Care symbols follow the GINETEX system in most export markets, and buyer-specific testing runs through laboratories such as SGS where a retailer programme requires it.
From Sample to Bulk: Locking the Specification Before the Order
The moment a programme becomes safe is not the purchase order. It is the point where both sides hold the same approved physical sample and the same version of the specification, and everything after that is execution.
The sequence Finetex Global runs on a men’s knitwear programme, with timelines given as indicative and subject to the latest quotation: tech-pack review, pattern making, grading, fit correction and fabric matching, then a fit or development sample in five to seven working days, followed by a graded size set in ten to twelve working days. Samples are built from the bulk fabric wherever relevant, so the handfeel approved at sampling is the handfeel received in bulk. Once a sample is approved, both parties hold a signed physical reference and specifications are version-controlled; any change resets the version number rather than being handled verbally.
In production, one named merchandiser owns the order and issues weekly written updates. Before packing, the final inspection report and photographs are shared with the buyer. If you want to see the line yourself, or send your own inspector, the factory is open at any stage of the run. Fabric-specific programmes such as the boxer briefs factory line show how that discipline applies to a single construction.
Send your current quotation for comparison. Finetex Global will break it into fabric, labour, trims and packing lines, confirm the minimum per colour and set out a sampling schedule: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Custom fabric development and sourcing for men’s knitwear programmes
- Men’s underwear manufacturing: fabrics, fits and quality control
- Boxer briefs factory: fabric-specific programmes and minimums
- Undershirt trends for basics brands: the subtle updates that matter
This page is part of our the apparel fabric selection guide, which covers the decisions before and after it.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day