
What is flock printing on fabric and how does it enhance textiles: A Production-Side Explanation
A 3,000-piece T-shirt programme goes to press with a chest logo signed off as a flat PDF. The first cartons land, the logo is patchy at…
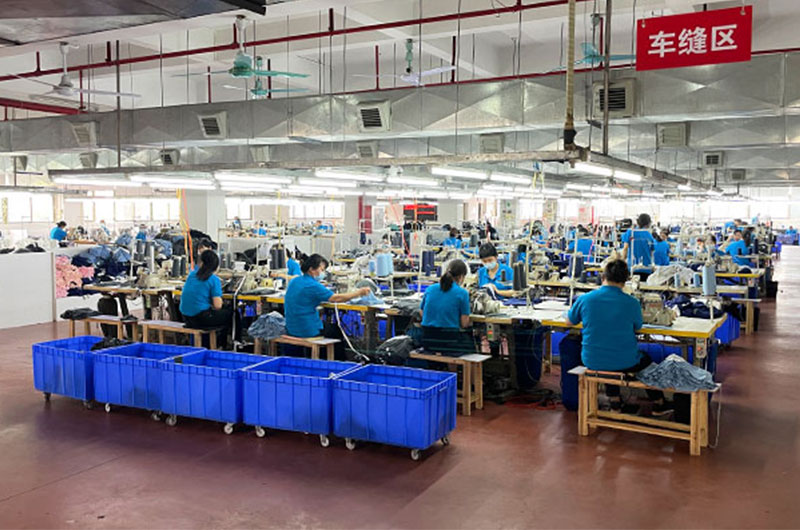
A 3,000-piece T-shirt programme goes to press with a chest logo signed off as a flat PDF. The first cartons land, the logo is patchy at the edges, and after two domestic washes the pile has flattened into a cracked film. Nobody argued about the artwork. The argument is about fibre, adhesive and cure. Flock printing is decided long before the press runs, at the moment someone writes “flocked logo” on a tech pack without stating pile height, coverage, the stretch of the base knit, or the wash test the decoration has to pass. This article explains what flock printing is, how a flock build changes the hand and look of men’s knitwear, and which specifications, tests and quantity decisions keep a decorated order from turning into a rejected batch.
The short answer on what flock printing does to a textile surface
Flock printing bonds short cut fibres onto fabric with an adhesive layer, producing a raised, matte, velvety decoration. On knitwear it enhances textiles by adding tactile dimension and colour depth at the surface, without changing the base knit, provided fibre type, adhesive, coverage and curing are matched to garment stretch, GSM and wash routine.
One-stop decorating: where flock sits inside a full knitwear programme
Flock is a finishing step, not a fabric, so it has to be scheduled against washing, pressing and packing instead of being bought as a separate item. On a men’s knitwear order it sits after cutting and sewing and before final finishing: the garment is stabilised, adhesive is applied, flock fibre is deposited, the build is cured, and the pieces then move through washing, trimming and inspection. The commercial point is sequencing. An enzyme or acid wash run after flocking can abrade the pile and dull the colour, while pressing a freshly flocked panel at full contact flattens it. Finetex Global, the trading brand of Finetex Textile Co., Ltd., runs fabric sourcing and development, sampling, cutting, sewing, printing, embroidery, finishing, packing and export documentation under one production plan, which is what allows that sequence to be controlled in a single routing; fabric knitting and dyeing run through long-term partner mills rather than being claimed as fully in-house. Practical note: ask any supplier to declare on the quotation where flocking happens in the routing and which finishing operations follow it.
That definition matters commercially because flock changes the surface rather than the structure, so it cannot be specified like a fabric and cannot be quality-checked like a seam. A flocked area behaves as a composite: knit, adhesive, fibre and heat history. Change any one of them between the sample and the bulk run and the decoration can look identical on the table and fail after the first wash. The method is used across upholstery, home textiles and womenswear as well as men’s knitwear, and this article stays inside men’s knitwear, where Finetex Global has produced for export since 2004. Everything below is written from the production side: what has to be fixed before sampling, what to measure, and what to put in writing.
From a good flock build to a repeatable one: the QC gates that decide
A flocked logo that passes on the first sample and fails at carton level is almost always a process-control failure, not an artwork failure. Flock has to be judged with the same discipline as the rest of the order: version-controlled specifications, an approved physical sample held by both parties, and checks at defined points rather than a single look at the end. Before cutting, Finetex Global inspects bulk fabric for shade continuity, shrinkage, weight per square metre and colour fastness, because flock adhesion and stretch behaviour follow the base knit. In-line QC runs at roughly 30% and 70% of the run, and final random inspection follows AQL 2.5 with a photo report before packing. The checks worth adding for flock are pile height and coverage consistency, adhesive strike-through on light knits, registration between colour layers, and cure verification. Practical note: test the wash performance of the flock on the bulk fabric and not on a lab swatch, and use an accredited third party such as SGS when the buyer’s programme calls for external testing.
Bringing creative ideas into production: the four variables that decide the result
Creativity in flock is bounded by four variables, and the earlier a design team knows them the fewer sample rounds it burns. Fibre choice sets the hand: viscose or rayon flock is soft, matte and the common apparel choice, nylon flock is crisper, more crush-resistant and slightly shinier, polyester flock holds light fastness well, and cotton flock reads matte and mild. Carrier choice sets the shape: direct flock deposits fibres into a printed adhesive on the garment, which suits open solid motifs, while a flock transfer builds the motif on paper or film first and heat-presses it, which suits fine outlines, small text and multi-colour builds. Coverage area sets cost and feel: a large solid area gives a dense velour surface but sits heavier on the knit, while an open motif protects the garment’s stretch. Cure discipline sets durability, because under-cured adhesive leaves fibres weakly bonded and over-cure flattens the pile. Practical note: supply vector art at final print size and approve a physical flock swatch built on the production fabric, not a screen preview.
Flexible flock routes by order size, knit weight and stretch
Route choice is a quantity and knit question before it is a design question. A pre-made flock transfer can run on a small first drop without a dedicated flocking set-up, but the motif stays within the shapes and colour layers the transfer supplier supports. Direct flock gives more freedom on large open areas and multi-colour builds, and becomes easier to control once the run justifies the set-up. Stretch is the second constraint: on elastane-blended knits the adhesive has to elongate with the fabric, or the flock cracks at flex zones such as shoulders and side seams. Weight matters too, since a light jersey surfaces adhesive differently from a 420 gsm French terry or a 500 gsm brushed fleece.
| Decoration route | Surface result | Colour and detail | Behaviour on stretch knits | Where it fits commercially |
|---|---|---|---|---|
| Flock transfer | Even velour pile, controlled height | Fine outlines and multi-layer builds | Depends on the transfer adhesive’s elongation | Smaller first drops, detailed crests and text |
| Direct electrostatic flock | Dense pile with open edges | Suits solid motifs and fewer colours per pass | Adhesive must be matched to the knit’s recovery | Volume runs, large chest or back coverage |
| Raised plastisol print | Rubber-like raised film, no fibre | Colour matching easier than flock | Cracks earlier on high-flex areas | Programmes that need colour accuracy over texture |
Practical note: put the route name, fibre, colour references and placement count on the tech pack, because “flocked logo” alone leaves the decision to whoever runs the press that day.
Cost-effective flock: what actually moves the per-piece price
Flock is priced on coverage, placements and colour layers rather than on the size of the order alone. A one-colour chest motif and a two-colour chest-and-sleeve build can share the same design file and still sit at very different costs, because each extra placement consumes press time, transfer stock and inspection attention. The levers that reduce cost without weakening the design are straightforward: consolidate placements, keep multi-colour builds inside the transfer formats the supplier already runs, use direct flock once the quantity justifies set-up, and avoid adding an inspection layer that duplicates an existing gate. Finetex Global issues a quotation within one working day with fabric, labour, trim and packing shown separately, holds quotations for 90 days, and credits sample charges against the bulk order; any figure quoted here is indicative and subject to the latest quotation, because flock cost moves with artwork and fibre selection. Practical note: ask for flock decoration as its own cost line rather than a bundle, so you can see what a second placement or a longer-cut pile actually adds per piece.
FAQ
What is flock printing in the textile industry?
It is a surface decoration method in which short cut fibres are bonded to fabric with an adhesive printed or coated as a motif. In production terms it is a finishing operation: adhesive is applied, flock is deposited, often in an electrostatic field so the fibres stand up, and the build is cured. Inside a garment programme it sits after sewing and before washing and packing, because heat and abrasion after flocking change the pile. On men’s knitwear it appears as logos, chest text and tonal motifs on T-shirts, sweats and heavier jersey styles.
What does flocked fabric look like?
Flocked fabric looks like velour or suede: a raised, matte surface that absorbs light instead of reflecting it, with soft edges where the fibres meet the base knit. Because the pile stands above the fabric, a flocked logo reads as physical rather than flat, and a colour often appears deeper than the same shade printed flat. On fine jersey the pile can hide the knit texture inside the motif. When a build is over-cured, weakly bonded, or applied to a knit it cannot stretch with, it looks cracked, flattened or dusty at the edges.
What is flocking in textiles?
Flocking is the broader finishing term for depositing short fibres onto an adhesive-coated surface. The same principle covers flat goods such as upholstery, nonwovens and home textiles, as well as printed motifs on apparel. Textile production usually separates surface flocking, where a whole panel or sheet receives a fibre coating, from motif flocking, where the adhesive is printed as a logo or pattern. Garment work is almost always motif flocking, which is why it belongs to the printing line rather than to a fabric mill’s finishing list.
Does flocked decoration survive industrial washing?
It can, when adhesive, fibre and cure are matched to the laundering conditions printed on the care label. Uniform, hospitality and retail programmes often wash far harder than a domestic cycle, so the tech pack should state the wash method, temperature and drying route, and the build should be tested against that method on the production fabric. Weak results usually trace to insufficient cure, an adhesive that cannot elongate with an elastane-rich knit, or a fibre chosen for appearance rather than laundering exposure. Test reports and certificates belong in the order file before any claim is published.
Which flock build to buy for value, higher-spec, sport and eco programmes
Buy the flock build, not the flock look. For a value programme, meaning a first drop with one logo on a cotton or cotton-blend tee, the sensible specification is a single-colour flock transfer or direct motif on stock fabric, with one placement and artwork that stays inside the shapes the transfer supplier already runs; that keeps set-up out of the price. For a higher-spec programme, layered flock over a printed base, longer-cut pile for a deeper velour hand, and a base knit such as modal or TENCEL set the decoration up to read as a considered surface, but each added colour layer has to be justified by the retail price. For sport and compression programmes, keep flock off the highest-flex zones, specify an adhesive that elongates with an elastane-rich knit, and test abrasion alongside washing. For eco-focused programmes, ask for OEKO-TEX Standard 100 documentation covering both flock fibre and adhesive, plus fibre chain-of-custody documents for the base fabric. Finetex Global is a Shenzhen men’s knitwear manufacturer and these recommendations come from men’s knitwear production; for women’s lingerie, denim or home textiles we do not claim production capability, though the same criteria work as an evaluation method.
Cost and MOQ breakdown: fabric at 45-60% and where the rest goes
On men’s knitwear, fabric commonly represents 45-60% of garment FOB, with labour, trim, packing and finishing making up the balance; that split is an indicative planning range and the real numbers come only from the current quotation. Flock sits in the finishing line, so it adds to decoration cost rather than fabric cost and does not change the MOQ logic of the base garment. Volume bands at Finetex Global run from 300 to 2,000 pieces per style in mixed sizes, with stock fabric from 300 pieces, a fully custom knit or dye lot typically from 1,000 pieces per colour, and roughly a third of programmes starting below 1,000 pieces per style – all indicative and subject to the latest quotation. The GSM and elastane trade-off matters just as much: T-shirt jersey in the range runs from 140 to 320 gsm and heavyweight fleece reaches 420 gsm French terry or 500 gsm brushed fleece. Denser knits hold pile better; higher elastane improves recovery but demands an adhesive that moves with the fabric.
Pre-production tests and QC gates worth writing into the tech pack
Flock performance should be verified against named methods rather than described in adjectives, because “durable” means nothing in a sourcing meeting. Before bulk release, test colour fastness to laundering on the flock and knit together using a defined method such as ISO 105-C06 or AATCC 61, add a crocking check such as AATCC 8 or ISO 105-X12 for dark piles, apply an abrasion method such as ISO 12947 where the motif sits in a high-contact area, and run the laundering procedure defined in ISO 6330 so wash temperature, detergent and drying are reproducible. Care labelling should follow GINETEX symbols and ISO 3758, and fibre content or care claims have to satisfy the disclosure rules in FTC textile labeling guidance and 16 CFR Part 303. Restricted substances in flock fibre and adhesive fall under OEKO-TEX Standard 100. The five gates that catch most flock failures are bulk fabric inspection before cutting, a flocked pre-production sample washed at label conditions, cure verification on the first run, in-line checks at 30% and 70%, and AQL 2.5 final inspection with a photo report before packing.
How to start: sampling, spec lock, then bulk production
The fastest route from artwork to a shippable flocked order is a fixed sequence, and skipping a stage is what creates rework. Start with a tech pack or a reference garment, including the flock artwork at final print size, placement measurements, fibre and adhesive expectations, the wash test to be met, and the base knit specification. Finetex Global produces a fit or development sample in about 5 to 7 working days and a graded size set in about 10 to 12 working days, both indicative and subject to the latest quotation, built from bulk fabric where the fabric is already selected. Once the flocked sample passes the agreed wash test, the specification is locked in a version-controlled document with an approved physical sample held by both parties. Bulk then runs with one named merchandiser per order and weekly written production updates. Practical note: send the reference, the artwork and the wash requirement in the first message, and the flock discussion starts from a costed position rather than a guess.
If you want the specification reviewed against your own target price, send the tech pack, reference sample or competitor garment. Finetex Global returns a costed quotation and sampling timeline, with all figures subject to the latest quotation: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- Custom fabric development for men’s knitwear programmes
- Men’s underwear manufacturing for private label brands
- Boxer briefs factory and fabric-specific programmes
- T-shirt wholesale for small brands: MOQ, pricing and minimums explained
It sits inside the wider the t-shirt printing and decoration guide, where the rest of the sequence is set out.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day