
Who are the leading Italian underwear manufacturers: supply chain and sourcing explained for buyers
A quotation lands, the per-piece cost is above the target, and the explanation offered is that the goods are Italian. Before you sign, you need to…
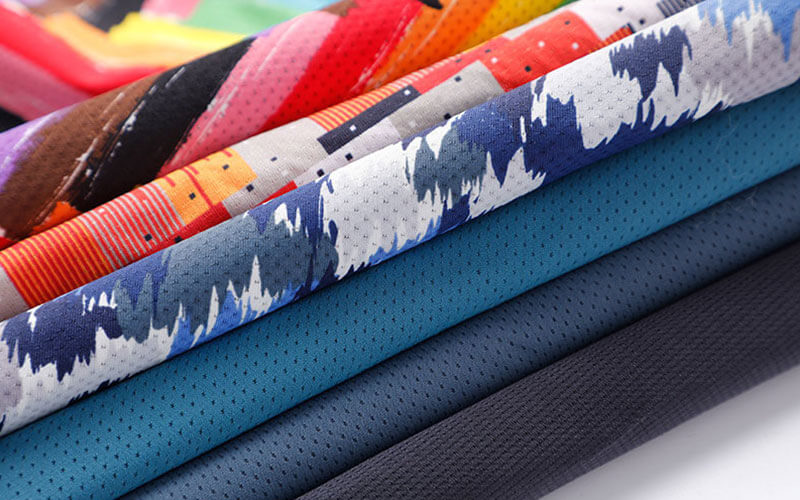
A quotation lands, the per-piece cost is above the target, and the explanation offered is that the goods are Italian. Before you sign, you need to know which part of the order is actually made in Italy: the knitting, the dyeing, the cut-and-sew, the finishing, or only the brand story wrapped around it. That answer decides whether you are buying a manufacturing relationship or a marketing position. This guide maps how Italian underwear supply chains are organised, what a factory name on a supplier list is worth, and how to verify capability before a launch date depends on it. Minimums, sampling windows and price figures below are indicative and subject to the latest quotation.
The short answer: where Italian underwear manufacturing actually sits
Italy’s underwear sector is a network rather than a shortlist. Its strength sits in brand management, knitting and finishing specialist mills, and small cut-and-sew workshops in northern districts such as Carpi. Large-scale cutting and sewing is usually contracted, often outside Italy, so a factory name is rarely published and must be verified per order.
What Italian underwear production does differently, and what it costs you
Italian programmes are bought for three things: design-led construction, small-batch flexibility and access to specialist mills. They are rarely bought for the lowest unit cost, and a quotation promising both deserves a closer look at the specification.
That structure has real depth behind it. Italian knitwear draws on dyehouses and mills that work in fine-gauge jersey, and on workshops able to execute short colour runs and detailed finishing that high-volume lines are not set up to handle. What it usually does not offer is a single site covering every stage under one production plan.
The practical consequence is that a supplier name describes a position in a chain, not a building. Ask separately for the fabric mill, the dyehouse, the cutting and sewing site, and the finishing and packing location, then establish which of those you are actually contracting with.
The construction difference shows up in details that are easy to specify and hard to fake: a waistband that recovers without twisting, flatlock seams that lie flat, and leg openings cut so the elastane does not pucker after washing. Those properties come from fabric weight, elastane content and stitch density set together, not from the country of origin alone.
In men’s basics, knit weights commonly sit between 120 and 220 gsm, and elastane content is traded against recovery, hand feel and cost. Fibre content, care instructions and origin claims also have to satisfy the destination market’s labelling rules; for the United States, the FTC’s textile labelling guidance and 16 CFR Part 303 set out what a label must state.
Ask for gsm, elastane percentage and dye-lot size in writing before price is discussed; those three numbers explain most of the gap between two quotations for the same style.
OEM and ODM in Italy: what a supplier will and will not take on
Below the large-brand tier, most Italian underwear production is subcontracting: an independent workshop cuts and sews to a brand’s own pattern. ODM work, where the supplier owns the block, is less common and usually confined to stock programmes.
The distinction shifts responsibility. In OEM you own the fit and pattern, and the factory executes your specification. In ODM you accept an existing pattern, fabric and grading, which shortens development but leaves the line closer to the market.
Minimums follow the fabric route, not geography. A workshop running stock fabric can start smaller, while a custom knit or dedicated dye lot pushes the opening order up. Indicative minimums start at 300 pcs per style on stock fabric and typically 1,000 pcs per colour on a custom knit, subject to the latest quotation.
Where your own specification is the asset, an OEM partner in a lower-cost knitwear region offers the same division of labour on a different cost base. Finetex Global, a Shenzhen manufacturer of men’s knitwear rather than an Italian producer, is named as a comparator; its men’s underwear manufacturing page sets out the programme scope.
Where men’s underwear capacity sits inside Italy
Capacity is a district story rather than a national one. Knitwear and jersey production clusters in the north, with Carpi in Emilia-Romagna the reference point most often cited for knitwear, while Prato, Biella and Como are associated with yarn, wool and silk specialities. Lombardy, Veneto and Tuscany host the smaller workshops that perform the actual cutting and sewing.
The district model cuts both ways. Distances between knitter, dyer and finisher are short, so a shade problem can be corrected in days rather than weeks, and trims, elastic and waistband specialists are close at hand. The friction is capacity: workshops are small, calendars tighten ahead of the main buying seasons, and a single supplier frequently controls only one step of the chain.
When you evaluate a supplier, sort each step into on-site capability or bought-in service. A cut-and-sew workshop that also owns its pattern room and finishing line removes two handoffs from your critical path, which is usually worth more than a marginal saving on assembly.
Reading an Italian underwear catalogue as a sourcing document
A catalogue is a sales document, not a specification, and treating it as the second thing is how specifications drift. It is useful for understanding a supplier’s construction style, fabric range and colour sense, and unsafe as the basis for a purchase order.
What a typical page gives you is a style code, a name, colour cards and sometimes a fibre composition. What it usually omits is the set of variables that decide whether the garment performs: fabric weight in gsm, elastane percentage, inseam and rise, waistband construction, stitch types at the seams, size-grading rules, permitted dye-lot variation, inspection level and packing format.
Convert each catalogue line into a written question. For a boxer brief, that means asking for the 3 to 9 inch inseam range, the pouch construction, the waistband elastic specification and the tolerance on a size medium. The answers become the opening section of a tech pack, which is the document a factory can actually quote and produce against.
Turning a custom request into a factory-ready brief
The brief controls the outcome, not the conversation that preceded it. A supplier who receives a reference garment and a clear specification can quote against a defined scope; a supplier who receives a photograph is quoting against an assumption that will surface later as a claim.
A workable brief carries measurement specs with tolerances, seam and stitch types, waistband elastic specification, label positions, care and fibre wording per destination market, and the packaging format. Care symbols follow a recognised scheme, and GINETEX publishes the international symbol set that most European labels use.
Two clauses deserve attention before production. First, pattern and grading ownership: if you paid for the block, the file and its revision history should be yours. Second, version control, so that the approved specification, not a later verbal adjustment, is what the line works to.
Expect the first sample to be an alignment tool rather than a finished product. Budget two or three rounds and treat each one as a checkpoint where fit, hand feel and construction are locked in sequence.
How to choose by programme type: value, premium, performance and sustainable
Sourcing decisions go wrong when a programme is judged by the wrong metric. A value multipack competes on landed cost and repeatability, a premium line competes on hand feel and finishing, a performance range competes on measured behaviour, and a certified range competes on traceability. Each points to a different fabric route, minimum and verification plan.
| Programme type | Fabric route | Weight and stretch | Minimum logic | Verification focus |
|---|---|---|---|---|
| Value and multipack | Stock cotton or cotton-rich jersey | Mid-weight, standard elastane | Lowest entry point per style | Shade continuity across the run |
| Premium | Modal, micro modal, pima or lyocell | Lighter weight, softer hand feel | Driven by dye-lot size | Finishing, waistband recovery, hand feel |
| Performance | Nylon, polyamide or polyester blends | Weighted for wicking and support | Custom knit, higher entry | Functional claims and wash durability |
| Sustainable and certified | Organic cotton, recycled polyester, certified fibres | Set by fibre availability | Custom knit or certified lot | Chain-of-custody documents |
Read the table as a set of trade-offs rather than a ranking. The premium route costs more per piece and can carry a higher minimum because the fabric has to be dyed to your colour, while the value route reaches a lower opening order by accepting a stock shade card. The performance route adds testing, because a wicking claim has to be supported by a report rather than by a fabric description.
A practical note for mixed ranges: build the core styles on one fabric family and reserve the speciality route for the hero style. Consolidating fabric across styles is usually the fastest way to reduce both minimums and unit cost without touching the fit.
Cost and MOQ arithmetic: fabric is the line that moves
On a men’s underwear style, fabric typically accounts for 45 to 60 percent of the unit cost, which is why the specification conversation is really a cost conversation. The remaining lines are quoted separately, so a breakdown showing fabric, labour, trim and packing as distinct items tells you where negotiation is possible and where it is not.
Weight and stretch trade against each other. A heavier knit consumes more grams per garment and raises the fabric line, while a higher elastane percentage improves recovery and shape retention at the cost of more demanding dyeing. Moving from 160 gsm to 180 gsm on a boxer brief is a small specification change and a measurable change in material consumption.
| Cost element | Share of unit cost | What drives it | Buyer lever |
|---|---|---|---|
| Fabric | 45 to 60 percent | gsm, elastane content, dye method, mill origin | Specify the weight and stretch the garment needs |
| Assembly labour | Quoted separately | Seam count, waistband application, inseam, decoration | Remove panels and seams that add no function |
| Trim and elastic | Quoted separately | Waistband construction, branding method, thread | Standardise trims across the range |
| Packing | Quoted separately | Polybag, hangtag, multipack, retail-ready format | Match packaging to the selling channel |
Minimum order quantity is set per style and per colour, not against total order value, so four colourways of one style is a different commitment from four sizes of one colourway. Indicative minimums run from 300 to 3,000 pcs per style, with stock fabric starting at 300 pcs and a custom knit or dye lot typically at 1,000 pcs per colour; all figures are indicative and subject to the latest quotation.
Tests and QC gates to fix before bulk production
Inspection gates belong in the purchase order before the first metre of fabric is cut; a defect found at the final audit is a claim, not a correction. Each gate should name what is checked and what happens on failure.
The first gate is bulk fabric, checked before cutting for shade continuity, shrinkage, weight per square metre and colour fastness. The second sits on the line at 30 and 70 percent of the run, catching fit or seam drift while correction is still cheap. The third is a final random inspection at AQL 2.5 with a photo report, plus a wash test on the assembled garment.
Skin-contact materials are commonly certified for harmful substances under OEKO-TEX STANDARD 100; the certificate is scope-based and has to name the material in your order. Chain-of-custody documents apply to bamboo, certified lyocell, recycled polyester and similar claims, and buyer programmes often require independent lab testing. Finetex Global documents these gates through its quality control process.
The backbone is unglamorous: a version-controlled specification and a physical approved sample held by both parties. Without both, every inspection becomes an argument about what was agreed.
How to start: sample, lock the specification, then release bulk
Three gates separate a reference garment from a shipped order, and each ends with a document. Sampling proves the construction, the approved sample locks the specification, and bulk release converts both into instructions.
Indicative timelines start at 5 to 7 working days for a fit sample and 10 to 12 working days for a graded size set, built from the bulk fabric where relevant. Minimums run from 300 to 3,000 pcs per style in mixed sizes, and around a third of programmes start below 1,000 pcs. A quotation usually returns within one working day, with fabric, labour, trim and packing shown separately. Figures are indicative and subject to the latest quotation; bulk lead time is confirmed at order placement.
Running the gates in order keeps a launch date realistic, because each removes an assumption before it becomes a cost. A buyer who approves fit, fabric and colour before bulk begins is buying a defined product, not a hope.
A supplier’s ability to hold a specification steady across those gates is worth assessing directly. Finetex Global publishes its capabilities and development process, covering pattern locking, sampling and export documentation.
FAQ
Which Italian underwear brands are most widely recognised?
Intimissimi and Tezenis, both part of the Calzedonia group, plus Yamamay and the luxury house La Perla, are the names most often associated with Italian underwear. Fashion houses such as Armani and Dolce & Gabbana also run underwear lines under their own labels. The important sourcing point is that a recognised brand is not a factory: a brand name tells you about demand and positioning, not about the site that cut and sewed a given order.
Who are the top clothing manufacturers in Italy?
The manufacturing base is mostly small and mid-sized family firms that do not market themselves to international buyers, which is why searching for a company name tends to return brands instead of factories. Production is concentrated in regional districts with a specific speciality in knitwear, wool, silk or jersey. Practical routes in are trade fairs, district industry associations and agent networks, followed by an audit of the specific site rather than of a group website. Expect to sign an NDA before a workshop shares its client list or pattern room.
Who makes high-quality underwear, and how do buyers verify it?
Quality is a property of process rather than of a country. Verification starts with a version-controlled specification and a physical approved sample held by both parties, then follows the fabric through inspection before cutting and the garment through checks at 30 and 70 percent of the run. A final random inspection at AQL 2.5 with a photo report, plus a wash test on the assembled garment, captures most of what a buyer would otherwise discover from returns. Ask for the reports, not the assurances.
Can a garment be labelled Italian if the fabric or sewing is imported?
Origin claims have to be substantiated and consistent with the rules of the market where the goods are sold. For the United States, fibre content and origin statements fall under the textile labelling framework described in the FTC’s labelling guidance and 16 CFR Part 303. Imported goods also pass through customs controls, and the US Customs and Border Protection import guidance sets out the entry requirements. Confirm the wording with your own compliance adviser for each market.
Is an Italian manufacturer the right route for a small first order?
Often it is the wrong fit for a first run, because the strength of the Italian route is craft and fabric rather than volume flexibility. A workshop working to your specification may hold a minimum that reflects a mill’s dye-lot size, and the calendar is tight around the main buying seasons. A common approach is to develop the line where the specification is easy to control at low volume, prove the fit and the selling rate, then place the volume programme once the specification has stopped changing.
Before you commit to a factory, ask for the cost breakdown. Send your specification to Finetex Global and the team will confirm what sits inside the price and what does not: contact Finetex Global. All figures are indicative and subject to the latest quotation.
Related resources
- V-neck undershirts under dress shirts: a spec for the commuter customer – neck rib control, GSM and shrinkage for a layered-wear programme.
- Men’s underwear manufacturer – OEM and private-label production scope across boxer briefs, trunks, briefs and undershirts.
- Capabilities and development process – pattern making, grading, sampling and export documentation under one production plan.
- Quality control – bulk fabric inspection, in-line checks, AQL 2.5 final audit and photo reporting.
- Contact Finetex Global – send a tech pack or reference garment for a costed quotation within one working day.
More factory-floor notes for brand owners

Sample Revision Limits: How to Control Underwear Development Cost and Calendar
A sample revision limit should control scope, not block necessary correction. The buyer and factory need to distinguish…
Read more →
Lab Dips and Strike-Offs for Underwear: Approval Steps That Prevent Delays
A lab dip approves a dyed textile shade; a strike-off approves printed artwork on the intended substrate. They…
Read more →
Color MOQ Planning: How to Share Fabric Across Multiple Underwear Styles
Color MOQ planning works best when a brand treats dyed fabric as a shared material platform rather than…
Read more →
Underwear Fabric Utilization: How Marker Efficiency Changes Unit Cost
Fabric utilization converts a fabric quotation into a garment cost. The calculation must account for pattern area, fabric…
Read more →
Open Costing for Men’s Underwear: Reading Fabric, Trim, Labor and Overhead Lines
An open-cost sheet is useful only when every line is tied to a measurable specification, a purchasing unit…
Read more →Global Apparel Sourcing Outlook 2026: Cotton, Freight and Supply-Chain Risk
A data-led 2026 apparel sourcing outlook on cotton balances, freight volatility, supplier diversification, lead time, compliance and practical…
Read more →Request a sample & pricing information
Send us your tech pack, target price or a reference sample — we reply with a quotation, a realistic lead time and a fabric recommendation within one working day.
- Free sampling plan & cost breakdown
- MOQ from 300 pcs per style
- Reply within 1 working day